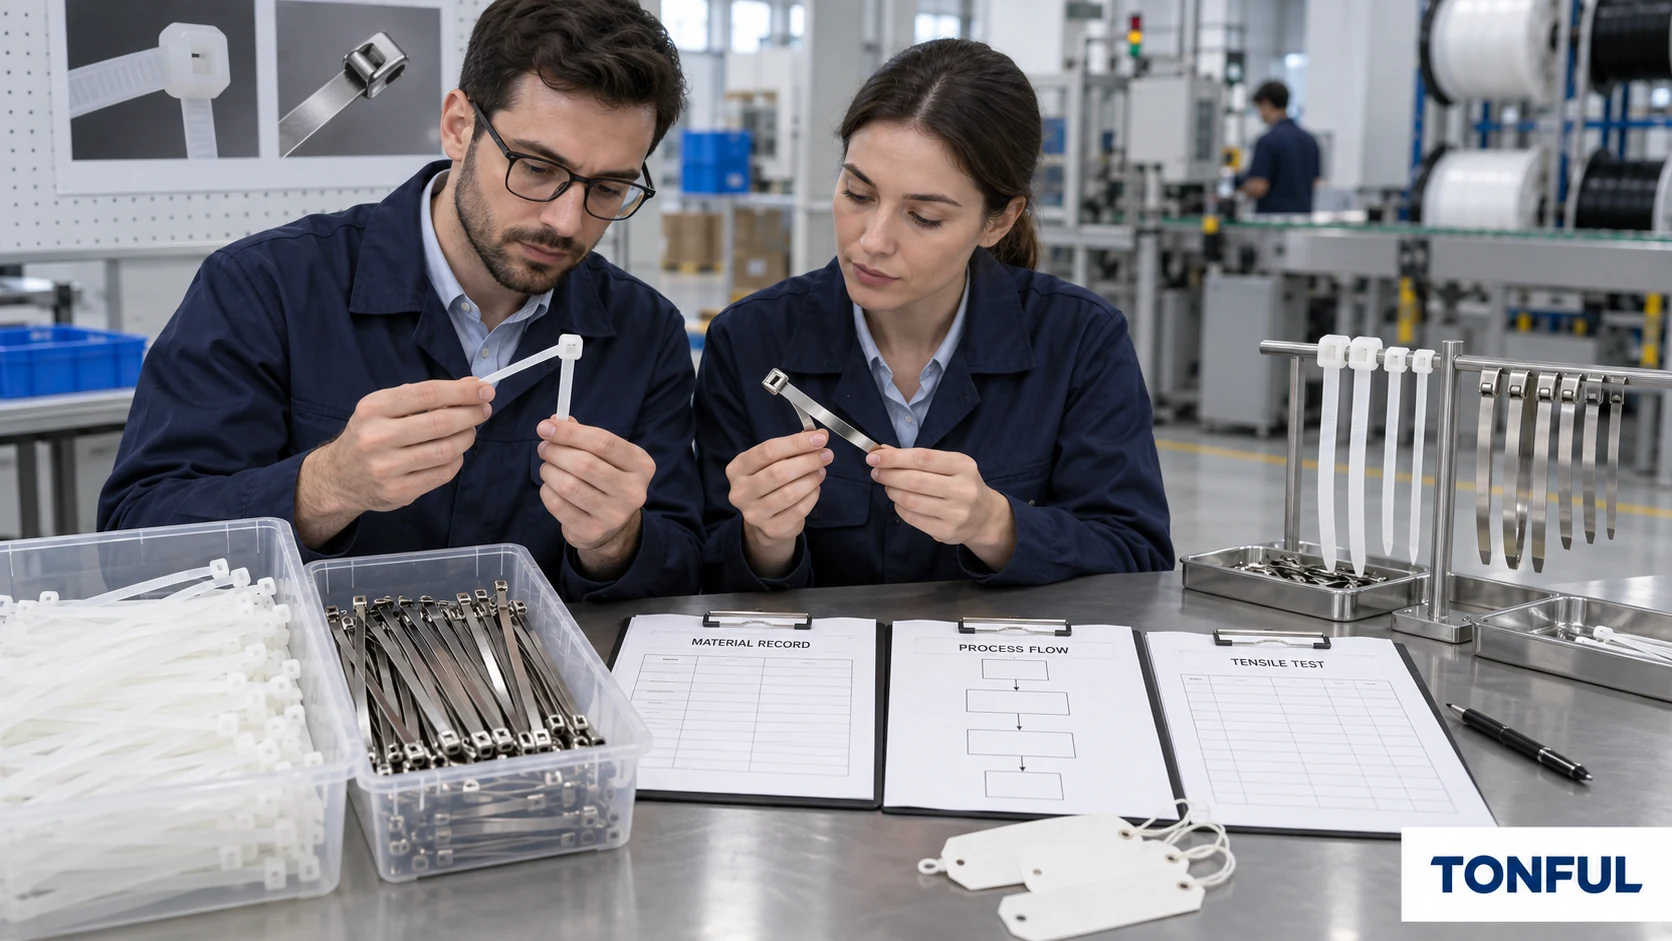
Approving a cable tie manufacturer should not depend on a showroom tour, one passing sample or an unchanged supplier part number. Cable tie performance is connected to resin or metal identity, tooling, tooth and lock geometry, conditioning, installation, testing, traceability and change control. A factory can produce an acceptable sample and still lack the controls needed for repeatable serial supply.
This checklist gives OEM buyers a risk-based, evidence-scored audit method. It does not certify a supplier or replace product qualification, production-intent sample approval and application testing.
Audit Scope, Criteria and Sampling
Define the legal entity, manufacturing site, products, materials, processes, shifts, outsourced operations and customer programs included. List audit criteria: contract requirements, drawings, approved specifications, quality-system procedures, customer-specific requirements and applicable standards. Unlisted scope is not automatically conforming.
ISO 19011 provides guidance for auditing management systems, audit programs and auditor competence. It is not a cable tie product specification and does not prove supplier approval. Apply its evidence-based and risk-based principles while using product-specific criteria.
Plan record samples before arrival. Follow one recent lot backward from shipment to finished testing, molding or forming, raw material and sub-suppliers. Follow one raw-material lot forward to all affected production and shipments. Observe production on the floor, interview authorized operators and challenge selected controls rather than reviewing procedures only.
Scoring and Decision Rules
Score each applicable question from 0 to 5:
| Score | Meaning |
|---|---|
| 0 | No effective control or evidence; requirement absent or contradicted |
| 1 | Ad hoc practice with major gaps and no reliable records |
| 2 | Partial control, inconsistently implemented or weak evidence |
| 3 | Defined and generally implemented with limited gaps |
| 4 | Effective control supported by sampled records and floor evidence |
| 5 | Robust, consistently effective control with monitoring and improvement evidence |
Weighted result = (item score / 5) x item weight. The 18 weights below total 100. For a justified N/A item, remove its weight from the denominator and normalize:
Normalized score = sum weighted applicable results / sum applicable weights x 100.
Use these finding classes:
- Critical: fraud, falsified records, loss of traceability for released product, unauthorized material/process change affecting approval, or another defined automatic rejection condition.
- Major: systemic failure or absence of a required control that can affect conformity; not offset by a high score.
- Minor: isolated lapse that does not demonstrate systemic breakdown.
- Observation: improvement opportunity with no demonstrated nonconformity.
- N/A: not applicable with documented product/process justification; excluded from the denominator.
- Not Evaluated: evidence was not sampled; receives no score and limits the approval scope.
A practical rule is: approve only when the normalized score meets the buyer’s defined threshold, no Critical exists, every Major is closed and all mandatory evidence is evaluated. Conditional approval must identify product, site, process, quantity or period, owner and expiry. The buyer must establish the threshold before the audit; this article does not invent one.
Executable Cable Tie Audit Matrix
| ID | Audit question | Weight | Evidence to sample | Sample size requirement | Finding / score / NC | Owner / due / closure evidence |
|---|---|---|---|---|---|---|
| CT-01 | Are customer drawings, revisions and specifications controlled at use points? | 5 | Contract review, master list, work instructions, obsolete-document controls | One active and one changed part | Complete during audit | Complete for each NC |
| CT-02 | Are material identities and approved sources controlled? | 7 | Resin/alloy/coating specs, certificates, incoming records, lot links | Three recent raw-material lots | Complete during audit | Complete for each NC |
| CT-03 | Are material changes, additives, pigments and regrind controlled? | 6 | Formulation controls, regrind limits, deviations, change approvals | Two products/colors and one change | Complete during audit | Complete for each NC |
| CT-04 | Are molds/forming tools, cavities and preventive maintenance controlled? | 6 | Tool list, cavity map, maintenance, repair and life records | Two tools plus one repaired tool | Complete during audit | Complete for each NC |
| CT-05 | Are molding or metal-forming parameters defined and monitored? | 7 | Setup sheets, parameter records, alarms and reactions | Three lots across shifts | Complete during audit | Complete for each NC |
| CT-06 | Are first-piece, tool-change, material-change and restart checks effective? | 5 | Approval records, challenge evidence, reaction plan | Three event records | Complete during audit | Complete for each NC |
| CT-07 | Are tooth, pawl, head, strap, lock, edge and coating characteristics controlled? | 7 | Drawings, inspections, optical records, defect samples | Two sizes and three lots | Complete during audit | Complete for each NC |
| CT-08 | Is nylon drying/conditioning or metal surface handling controlled? | 6 | Drying/conditioning records, packaging, storage, surface protection | Three lots and floor observation | Complete during audit | Complete for each NC |
| CT-09 | Are installation and cutoff tools validated where supplied or specified? | 4 | Tool specification, settings, verification, blade control | Two tools and two tie families | Complete during audit | Complete for each NC |
| CT-10 | Are dimensional, locking and loop-tensile tests controlled? | 7 | Methods, equipment, sample records, raw curves, failures | Three lots and one test witness | Complete during audit | Complete for each NC |
| CT-11 | Are environmental/qualification tests traceable to exact products? | 5 | Plans, sample allocation, chamber logs, reports, approvals | Two qualification reports | Complete during audit | Complete for each NC |
| CT-12 | Are measurement systems, calibration and MSA suitable? | 6 | Calibration, status labels, GR&R/MSA where applicable | Five devices plus one MSA | Complete during audit | Complete for each NC |
| CT-13 | Do PFMEA, Control Plan, work instructions and records align? | 5 | Process Flow, PFMEA, Control Plan, WI, inspection records | One complete active chain | Complete during audit | Complete for each NC |
| CT-14 | Are SPC, process capability and reaction plans used where applicable? | 4 | Charts, Cp/Cpk or alternative evidence, reactions | Two key characteristics | Complete during audit | Complete for each NC |
| CT-15 | Are nonconforming product, rework and corrective actions controlled? | 5 | Quarantine, concessions, rework approval, retest, 8D | Three NCs and two complaints | Complete during audit | Complete for each NC |
| CT-16 | Is bidirectional lot traceability demonstrated by a mock recall? | 6 | Raw-to-finished and finished-to-raw records, reconciliation | One live trace drill | Complete during audit | Complete for each NC |
| CT-17 | Are sub-suppliers, outsourced processes and changes controlled? | 4 | Approved list, performance, coating/plating controls, notifications | Two critical suppliers | Complete during audit | Complete for each NC |
| CT-18 | Are delivery, PPM, returns, repeat complaints and closure effectiveness reviewed? | 5 | Scorecards, warranty, delivery, previous audits, recurrence | Prior 12 months or agreed period | Complete during audit | Complete for each NC |
For every sampled row, use a separate finding record rather than writing an unexplained score into the matrix. This keeps the overview readable while retaining the evidence needed for a defensible conclusion:
| Finding-record field | Entry to capture |
|---|---|
| Audit ID and question | CT number and controlled audit criterion |
| Evidence ID and sample size | Record, interview or observation reference; planned versus actual quantity |
| Requirement and finding | Exact criterion, objective evidence and affected lot/process |
| Score and NC level | 0–5 or justified N/A/Not Evaluated; Critical/Major/Minor/Observation |
| Owner and due date | Named responsible person and agreed closure deadline |
| Closure verification | Containment, root cause, permanent action, sampled effectiveness evidence, reviewer and date |
Do not score Not Evaluated as zero or omit it from the conclusion. A missing mandatory audit area requires follow-up before full approval; N/A requires a reason and approval, not a blank cell.
Audit the Quality Planning Chain
Select one cable tie and trace Customer Requirements -> Project/APQP Plan when required -> Design/Process Risk -> Process Flow -> PFMEA -> Control Plan -> Work Instruction -> Inspection Record -> Release. Each document should carry consistent product characteristics, methods, frequencies and reaction plans.
Where customer or contract requirements call for APQP, PPAP, core tools or customer-specific records, verify the applicable evidence. Do not declare those methods mandatory for every cable tie project. The supplier must be able to explain what governs approval and how changes reopen it.
The cable tie manufacturing process guide can help buyers recognize molding stages, while the cable tie moisture and storage guide provides questions for nylon handling.
Review Product-Specific Manufacturing Controls
Polymer Cable Ties
Verify resin receipt, identity, storage, drying where required, color/additive control, regrind authorization, molding setup, cavity traceability, tooth and pawl inspection, deflashing, conditioning, packaging and lot release. Challenge mixed-material prevention and response to a cavity-specific defect.
Observe whether parameter limits are controlled or merely written after production. Ask how an operator reacts to incomplete fill, flash, brittle handling, color drift, tooth damage or poor locking. Review cavity-level records when one defect can be isolated to part of a mold.
Stainless and Coated Cable Ties
Trace strip or wire alloy, lock components, forming, edge condition, coating, cutting and packaging. Verify outsourced coating or surface processing controls. Review burr, lock seating, strap slip and coating-damage criteria. The 304 versus 316 stainless cable tie guide provides corrosion-selection context, not supplier approval.

Sample objective evidence from the production floor and records; a procedure alone does not prove implementation.
Test Laboratory, MSA and Release
Witness a loop-tensile or locking test. Check specimen identity, conditioning, fixture, speed, equipment range, accuracy, calibration and failure-mode recording. Compare the work instruction with actual practice and raw machine output. Review invalid-test and retest rules.
For measurement systems, verify calibration traceability and current status. Require MSA or GR&R where the customer, risk or process requires it; do not demand one study for every visual check. For key process data, confirm that SPC or alternative monitoring has defined reaction rules and that out-of-control events lead to containment.
The cable tie tensile strength guide explains why test method and conditioning matter. Product qualification does not replace daily release controls, and an end-of-line test does not compensate for uncontrolled material or tooling.
Traceability, Recall and Change Control
Run a timed trace exercise. From a shipped lot, identify finished inspection, date/shift, machine, tool/cavity where used, material lot, conditioning, packaging and affected shipments. From a raw lot, identify every product and customer potentially affected. Reconcile quantities and explain scrap, work in process and retained stock.
Review notification and approval rules for resin/alloy source, additives, color, coating, dimensions, tooth/pawl or lock geometry, mold/tool, manufacturing site, test method, sub-supplier and packaging. An unchanged SKU is not proof of unchanged construction.
Automatic rejection examples should be agreed before the audit and may include falsified records, unauthorized critical change, inability to trace released lots, deliberate shipment of known nonconforming product or refusal of required evidence.
Corrective Action and Closure
Each nonconformity must identify requirement, objective evidence, affected scope and classification. The supplier should contain product, determine root cause, define permanent correction, update risk and control documents, verify implementation and demonstrate effectiveness. Attach owner, due date and closure evidence.
Do not close a Major from a revised procedure alone. Sample implementation records and observe the changed process. Repeated findings, overdue 8D reports and ineffective recurrence prevention belong in the supplier-performance score.

Normalize scores for justified N/A items, but never allow a high total to cancel a Critical or open Major finding.
Approval Decision
Report the normalized score, applicable weight, findings, unassessed scope, knockout status and product/site limitations. A high score with an open Major is not approval. Not Evaluated areas must restrict the conclusion. Conditional approval requires a controlled deviation, owner, expiry, quantity or product boundary and closure plan.
Supplier audit approval also does not approve a cable tie for service. Keep supplier status, sample approval, product qualification and production release as separate decisions.
Work With TONFUL
TONFUL’s cable tie range can be reviewed against your controlled specifications, sample plan and supplier-audit requirements. Share the product families, factory scope, required documents, test evidence and customer-specific criteria so the audit and sample review can be prepared without unsupported assumptions.