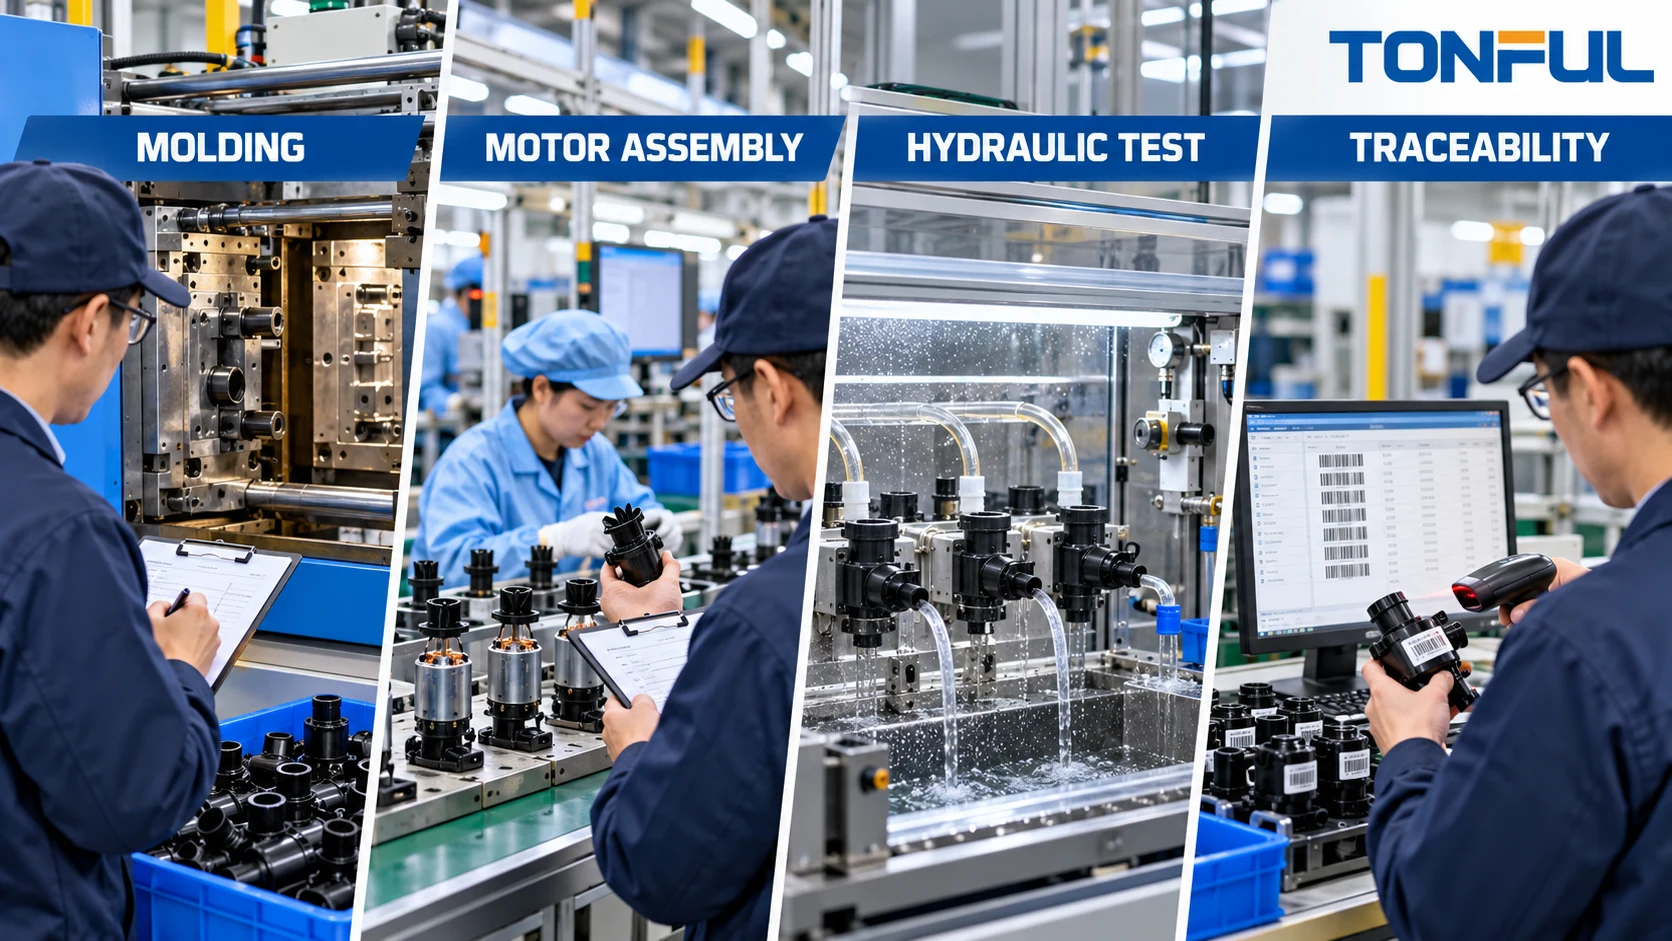
Approving a washer pump manufacturer should not depend on a showroom tour, supplier questionnaire or one passing sample. A reliable audit follows customer requirements through design records, purchased materials, molding, motor and impeller assembly, sealing, electrical connection, hydraulic testing, packaging and field performance. It must also state how evidence is sampled, scored and closed.
This checklist uses a normalized 100-point model with 18 product-specific questions. A high score cannot cancel an automatic rejection or open Major nonconformity. Product qualification, sample approval and vehicle validation remain separate decisions.
On this page: Audit method | Scoring | 100-point matrix | Process chain | Product controls | Closure
Audit Scope, Method and Evidence
Define the factory, product family, manufacturing processes, outsourced operations, shifts and customer requirements before the visit. Audit criteria may include the contract, approved drawings, quality agreement, applicable management-system requirements and customer-specific procedures. An unvisited process or shift cannot be assumed conforming.
ISO 19011:2026 provides guidance for auditing management systems, managing audit programs and evaluating auditor competence. It is not a washer-pump product specification, test method or proof of supplier approval. Use its evidence- and risk-based approach while applying project-specific technical criteria.
For each question, record the audit trail, evidence ID, sample size, finding, score and nonconformity level. Combine interviews, shop-floor observation, record review and trace-forward/trace-back checks. Select samples across lots, shifts, cavities, operators and change events rather than accepting only supplier-selected “best” records.

Conceptual illustration only—not an acceptance standard or laboratory micrograph. Audit criteria and sample sizes must be defined for the project.
Scoring and Decision Rules
0–5 Score Anchors
| Score | Meaning |
|---|---|
| 0 | No effective control or evidence; critical requirement absent |
| 1 | Ad hoc control with serious gaps and no reliable implementation evidence |
| 2 | Partly defined control, inconsistent execution or weak records |
| 3 | Defined and generally implemented control with limited gaps |
| 4 | Effective control supported by sampled records and reaction evidence |
| 5 | Effective, sustained and risk-based control with trend and improvement evidence |
Weighted result for each item equals score ÷ 5 × applicable weight. The matrix weights total 100. If an item is genuinely not applicable, document the reason and exclude its weight from the denominator:
Normalized score = sum of earned applicable points ÷ sum of applicable weights × 100.
Not Evaluated receives no score and restricts approval scope; it is not the same as N/A. Use Conforming, Minor, Major, Critical, Observation, N/A or Not Evaluated consistently.
Decision Thresholds
- Approved: normalized score at or above the project threshold, no Critical finding, no open Major and all mandatory scope evaluated.
- Conditional: limited product/factory/process/time scope with named deviations, owner, due date and closure evidence.
- Rejected: automatic disqualifier, unresolved Critical, unacceptable score or evidence integrity failure.
Set the numeric approval threshold before the audit. Do not adjust it after seeing results.
Nonconformity Levels and Knockouts
A Critical finding creates immediate product, safety, legality or evidence-integrity risk. A Major is a systemic failure or missing control capable of affecting conformity. A Minor is an isolated lapse that does not indicate system breakdown. An Observation is an improvement opportunity, not disguised nonconformity.
Automatic rejection examples include falsified records, loss of lot traceability, unauthorized product or material change, shipment of rejected product, inability to contain a serious defect, or refusal to provide required evidence. These act independently from the weighted score.
100-Point Washer Pump Audit Matrix
| ID | Audit question | Weight | Evidence to sample | Minimum sampling direction |
|---|---|---|---|---|
| 1 | Are customer requirements, drawings and revisions controlled? | 6 | Contract review, drawings, change log | Current product plus one prior revision |
| 2 | Are APQP/project risks and approvals managed where required? | 6 | Timing, risk reviews, customer approvals | One current and one completed project |
| 3 | Are special characteristics transferred through documents? | 5 | Drawing, PFMEA, control plan, WI, record | Trace three characteristics end to end |
| 4 | Are resin, molding parameters, cavity and tool maintenance controlled? | 6 | Material lots, setup, cavity records, PM | Three lots across cavities/shifts |
| 5 | Are motor, brush, commutator and winding inputs controlled? | 6 | Specifications, incoming data, supplier lots | Three purchased lots or builds |
| 6 | Are impeller/rotor assembly and balance/process settings controlled? | 6 | Fixtures, settings, verification, reaction | Three setups including a changeover |
| 7 | Are seals, grommets, lubricants and fluid-contact materials controlled? | 6 | Approved list, lot trace, shelf life | Three material lots and storage checks |
| 8 | Are terminals, connectors and polarity mistake-proofed? | 5 | Cavity map, poka-yoke, challenge records | Start-up plus three production samples |
| 9 | Are assembly force, depth, welding or joining parameters controlled? | 6 | Parameter logs, limits, alarms | Three lots and one restart/change event |
| 10 | Does end-of-line testing cover required electrical and hydraulic functions? | 6 | Program revision, fixture, limits, rejects | Witness test and trace three records |
| 11 | Are flow, pressure, current, leakage and noise methods controlled? | 6 | Methods, MSA, calibration, samples | One method study plus three samples |
| 12 | Are endurance and environmental qualification records traceable? | 5 | Plan, sample allocation, raw data, report | One approved project and one change |
| 13 | Are measurement systems, calibration and GR&R addressed? | 5 | Calibration, MSA, gauge status | Critical gauges plus overdue search |
| 14 | Are SPC/capability and reaction plans used where appropriate? | 5 | Charts, capability, alarms, containment | Two characteristics across recent lots |
| 15 | Are nonconforming product, rework and revalidation controlled? | 5 | NCR, rework authorization, retest | Three cases including one repeat issue |
| 16 | Are packaging, labels and mixed-part prevention effective? | 5 | Pack spec, scans, line clearance | Witness changeover and finished stock |
| 17 | Are traceability, change control, sub-suppliers and recall drills effective? | 5 | Trace drill, PCN, supplier controls | One forward/backward drill and one change |
| 18 | Are supplier performance and corrective actions effective? | 6 | PPM, delivery, returns, 8D, recurrence | Twelve-month trend and three complaints |
The total weight is exactly 100. Add columns in the working audit form for Risk | Evidence ID | Sample Size | Finding | Score | NC Level | Owner | Due Date | Closure Evidence.
Verify the Quality Planning Chain
Follow Customer Requirements → APQP/Project Planning → Design and Process Risk → PPAP or Customer Approval → Serial Production Controls where contractually required. Do not imply that every aftermarket project must use PPAP or a particular automotive core tool. Instead, verify the applicable customer and contractual records.
For the shop floor, trace Process Flow → PFMEA → Control Plan → Work Instruction → Inspection Record. Select a critical characteristic such as inlet geometry, outlet position, seal interface, terminal polarity or hydraulic output and confirm that the same definition, limit and reaction logic appear throughout the chain.
Review first-piece, tool-change, material-change, cavity-change and downtime-restart approvals. Verify that a failed check triggers containment, last-known-good analysis and documented disposition rather than a simple adjustment with no product review.
Washer Pump-Specific Process Controls
Molding and Fluid Interfaces
Housing and impeller molding can affect dimensions, sealing, balance and crack resistance. Audit resin identity, drying where required, cavity traceability, process windows, tool maintenance and dimensional inspection. A generic resin family name does not prove the exact grade or fluid compatibility.
Motor and Rotating Assembly
Review motor-source approval, winding or purchased-motor controls, brush and commutator evidence, shaft/impeller assembly, runout or balance method and contamination control. Confirm how reversed polarity, incorrect component mix or assembly depth is prevented.
Sealing and Joining
For welding, staking, pressing, adhesive or other joining, verify parameter control and destructive or nondestructive validation as applicable. Seal installation must control orientation, damage, lubrication, shelf life and mating dimensions. Leak-test fixtures need challenge parts or a defined verification method.
Electrical and Hydraulic End-of-Line Test
Witness the end-of-line sequence. Confirm product identification, program revision, connector/polarity check, startup, current, flow or pressure proxy, leakage and dual-outlet direction where applicable. Review test coverage rather than assuming “100% tested” means every requirement is measured.
Use controlled factory test methods rather than a planned content URL as evidence. Existing TONFUL pages for automotive electrical connectors, custom wire harness assemblies and blade fuses provide related product context only. Its wiper switch diagnostic guide helps define command-side boundaries but does not prove pump conformity.

Conceptual illustration only—not an acceptance standard or laboratory micrograph. Audit findings require sampled factory evidence.
Measurement, Capability and Reaction
Check calibration traceability and gauge status at point of use. Review measurement-system analysis for critical dimensional, electrical and hydraulic results. A calibrated instrument can still be unsuitable if resolution, fixture variation or operator method is inadequate.
Where statistical control is appropriate, examine stability before capability. Confirm subgroup logic, specification source, Cp/Cpk or other agreed evidence, and reaction to out-of-control or incapable conditions. Do not demand a capability index where data type or process does not support it; document the alternative control.
Witness challenge-part testing for error-proofing and end-of-line fixtures. Verify challenge frequency, secure storage, expiration and reaction after a failed challenge.
Traceability, Change and Performance
Perform a bidirectional trace: finished pump to motor, resin, seal, terminals, assembly line, shift and test record; then one input lot forward to affected finished goods and customers. Time the exercise and compare recovery with the agreed requirement.
Review sub-supplier approval and changes for motors, brushes, seals, terminals, resin and outsourced processes. Unauthorized changes are not acceptable even if dimensions appear unchanged. Examine delivery performance, incoming/customer PPM where applicable, field returns, warranty claims, complaint recurrence, 8D closure timeliness and repeat audit findings.
The TONFUL automotive washer pump category confirms the product-family context for sourcing. It does not independently prove that a specific factory, model or process has passed this audit.
Corrective Action and Approval Scope
Every nonconformity needs objective evidence, requirement, risk, containment, root cause, permanent action, owner and due date. Closure requires implementation evidence and effectiveness verification; a promised action or revised document alone may be insufficient.
A conditional approval must name the factory, product, process, volume/time boundary and excluded scope. A high normalized score cannot override an open Major. Not Evaluated areas remain outside approval. Re-audit when changes or performance risk justify it.

Conceptual illustration only—not an acceptance standard. The buyer must approve thresholds and automatic rejection rules before the audit.
Work With TONFUL
Share the product scope, vehicle/application requirements, drawings, expected evidence and audit criteria with TONFUL before supplier review. TONFUL can organize the relevant product and process discussion without treating a website claim as approval evidence. Release should follow the completed audit, sample validation and project-specific qualification records.