Bulk heat shrink tubing purchasing is not simply a larger version of a sample order. Reel length, joints, usable yield, cut tolerance, lot identity, packaging, storage, incoming inspection and supplier changes can affect production cost long after the unit price is agreed. A product that passes an initial sample can still disrupt cutting equipment or assembly if routine supply is inconsistent.
This guide helps OEM buyers, harness manufacturers, distributors and contract assemblers define bulk heat shrink tubing, approve production-intent samples and maintain control after launch. Exact ratings, tests, limits, MOQ and lead time must be confirmed for the quoted product and project rather than assumed from a catalog family.
On this page: Specification | Samples | Cost | Packaging | Incoming | Changes
Freeze an Equivalent Purchasing Specification
Define the application and exact product before comparing bulk quotations. Record material, wall construction, color, supplied inside diameter, maximum recovered inside diameter, recovered wall, shrink ratio, longitudinal change and supply format. Include cut length and tolerance for pieces, or reel length and permitted joints for continuous supply.
The tube must pass over the largest assembly feature and recover onto the smallest substrate across tolerance. A nominal size or ratio alone does not prove fit. The heat shrink sizing guide explains pass-over and recovered-fit calculations, while the material guide compares polymer families.
Translate “industrial,” “automotive,” “marine” or “flame-retardant” into evidence-based requirements. State the applicable drawing, customer specification, standard edition, temperature or electrical requirement, fluid exposure, UV, abrasion and assembly-level seal need. Identify mandatory characteristics separately from supplier proposals.
Lock the Approved Scope
The purchase specification should identify the approved supplier product designation, revision, manufacturing site, material or formulation reference, color, construction and packaging. If multiple sizes or colors are grouped under one approval, document the technical basis. Do not automatically extend a report from one wall, color or size to the entire family.
UL’s official insulating tubing testing and certification overview explains that tubing categories, optional properties and conditions of acceptability vary. Request evidence for the exact product scope; do not treat a recognition mark or broad certificate as proof of every catalog claim.
Approve Production-Intent Samples
Samples should represent the planned resin or compound, pigment, adhesive liner, extrusion, cross-linking, expansion, printing, cutting and site. Ask the supplier to disclose any difference between prototype and production. A hand-selected laboratory sample cannot establish normal process capability.
Create a sample plan by size, color, construction and application risk. Measure supplied and recovered dimensions, wall, length and longitudinal change as applicable. Evaluate recovery behavior with the approved heat source and installation window. For adhesive-lined tubing, inspect liner distribution, substrate wetting and assembly geometry rather than accepting a visible end bead as universal sealing proof.
Use independent specimens where tests are destructive or prior conditioning could affect the result. Record lot, specimen ID, method, equipment, conditioning, raw result, acceptance source and reviewer. The heat shrink testing guide provides a reusable evidence structure.
Separate Approval Stages
Use distinct status terms:
| Approval stage | Evidence | Purchasing meaning |
|---|---|---|
| Catalog candidate | Data sheet and preliminary fit review | Not approved for production |
| Development sample | Early material or process sample | Evaluation only; differences recorded |
| Production-intent sample | Planned site, material and process | Eligible for validation |
| Sample approved | Named samples meet agreed checks | Does not approve unlimited production |
| Production approved | First article and required evidence accepted | Release only within approved scope |

Clear approval stages prevent development samples from being mistaken for unrestricted production supply.
Calculate Usable Yield and Total Cost
Price per meter is useful only when the meter is usable. Define whether quoted length excludes leaders, damaged ends, joints and setup waste. Record permitted reel-length tolerance and how shortages are handled. For automated cutting, confirm spool dimensions, winding tension, payout direction, telescoping, flattening and minimum bend effects.
Calculate expected usable yield:
Usable yield = accepted cut pieces / theoretical cut pieces from received length x 100
The theoretical count should include the controlled cut length and known machine kerf or process allowance. Do not hide start-up scrap, splice removal, distorted sections or rejected print inside an unexplained efficiency factor.
Build total accepted cost:
Total cost per accepted piece = (material + freight + receiving + cutting + inspection + scrap + rework + inventory carrying cost) / accepted pieces
Avoid double counting. If material cost has already been divided by accepted yield, do not add the same scrap material again. Separate one-time qualification or tooling charges and amortize them over a realistic approved volume, not an optimistic lifetime forecast.
Evaluate Price Breaks Responsibly
Ask for MOQ, reel or package quantity, price breaks, currency, Incoterm, quotation validity and delivery location. Confirm whether different sizes, colors or prints can be combined for MOQ. A volume discount can be offset by aging, storage space, obsolete labels or a design change before inventory is consumed.
Use expected, conservative and stress scenarios for annual demand, yield and freight. Compare suppliers on equivalent accepted product and evidence scope, not only quoted length.
Control Reels, Cuts, Packaging and Labels
Bulk supply may arrive on reels, spools, coils, sticks, bags or precut kits. Specify reel core, flange diameter, winding direction, maximum package mass and line-side handling constraints. State whether joints are allowed, the maximum number, required identification and minimum uninterrupted length. Unmarked joints can enter an automatic cutter and create short or defective assemblies.
For precut tubing, define length tolerance, squareness, deformation, burr or split criteria and count method. For printed pieces, control artwork revision, orientation, print location, contrast, legibility, permanence and sequence. For adhesive-lined products, packaging should prevent blocking, contamination and deformation under expected storage conditions.
Every primary package should carry the required part number, revision, size, color, construction, quantity or length, supplier lot, manufacturing date, site and purchase reference. Barcode format must match the buyer’s system when required. Do not invent a shelf life: request the supplier’s documented storage conditions, basis and expiration or retest policy for the exact product.

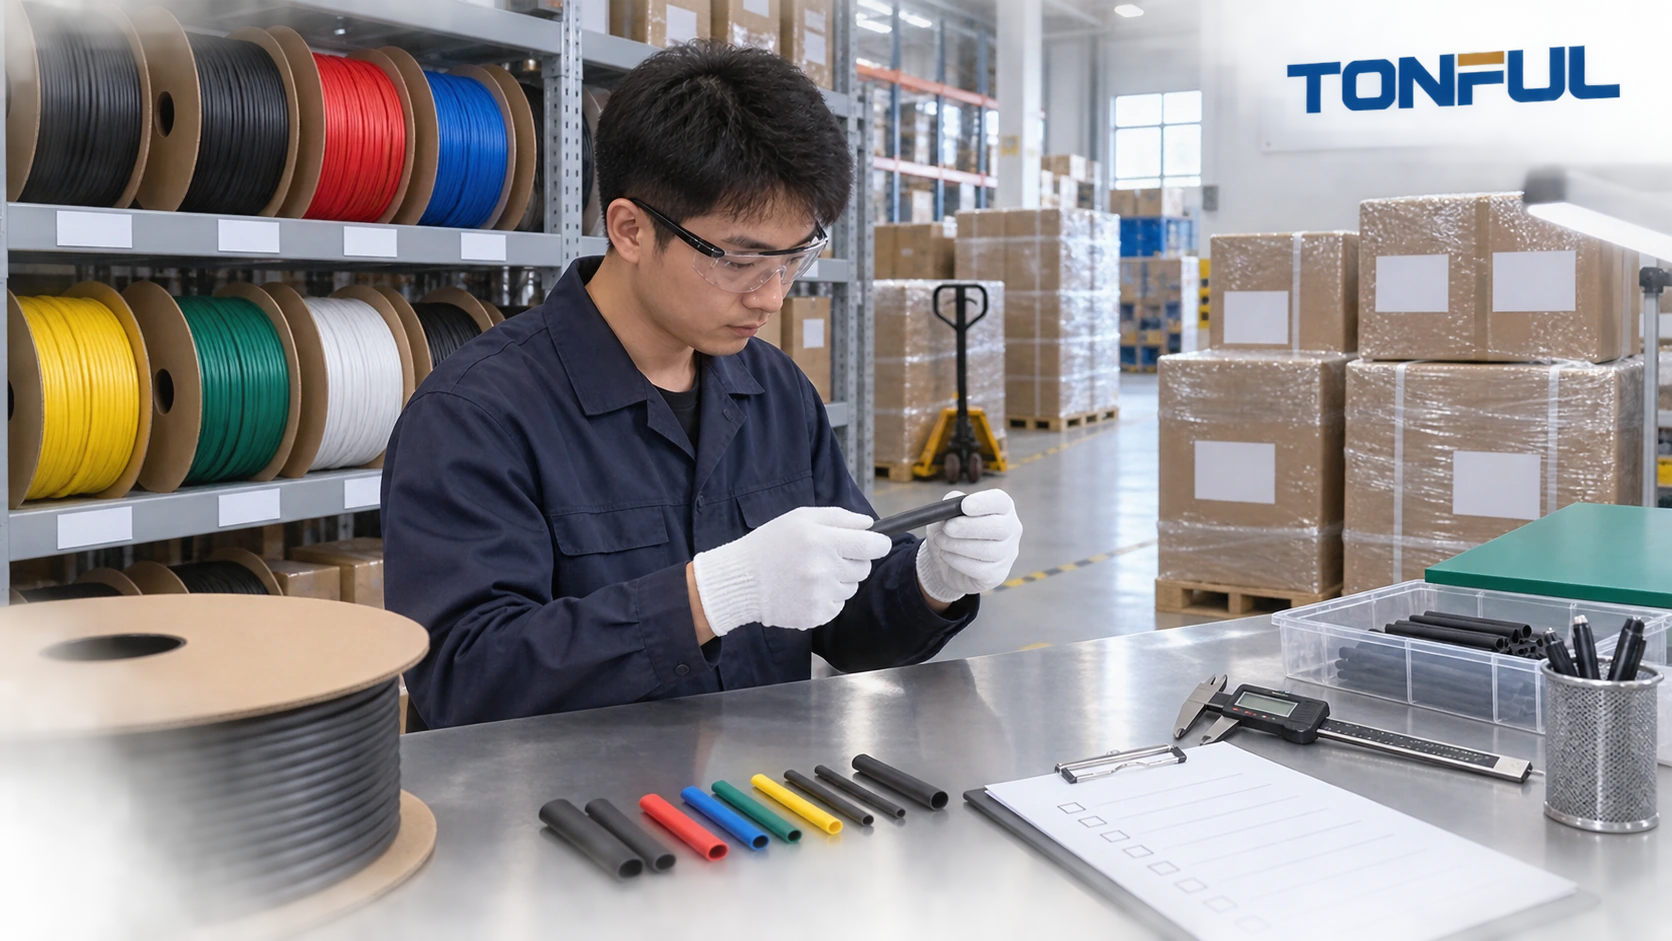
Bulk packaging should make reel identity, joints, quantity and handling conditions visible before the material reaches the cutter.
Build Risk-Based Incoming Control
Incoming inspection should confirm identity before testing performance. Verify purchase order, supplier part, revision, material/construction, size, color, lot, quantity and package condition. Quarantine mixed labels, damaged reels, moisture exposure or broken traceability.
Select checks from risk and supplier performance. Possible characteristics include supplied ID, recovered ID, wall, cut length, appearance, print, recovery and selected document review. Use a documented sampling plan, measurement method, calibrated equipment and reaction plan. Do not silently change sampling frequency because recent lots have passed.
Retain Comparable Data
Trend results by supplier, product, size, color, line, material lot and date where data are available. Monitor shortages, reel joints, cutting yield, dimensional variation, assembly rejects and complaints. A shift within specification may still warn of process drift.
Keep retention samples when required by the control plan. Define quantity, identification, storage and retention period. A retained piece without its original lot and conditions has limited investigative value.
Use supplier certificates as supporting evidence, not a replacement for all receiving controls. Verify that each certificate identifies the shipped lot and required characteristics. Resolve inconsistent units, methods or revisions before release.
Maintain Lot Traceability and Inventory Discipline
The buyer should be able to trace received material to supplier lot and identify where that lot was consumed. Avoid relabeling that destroys the original reference. When reels are split, preserve parent-child identity. When pieces are kitted, maintain the tubing lot in the kit or production record as required.
Apply first-in-first-out or documented expiration control according to the product’s storage requirements. Protect tubing from heat, sunlight, contamination, crushing and conditions that affect the liner or print. Review slow-moving stock after changes rather than automatically issuing it.
Run a trace exercise periodically: select one finished assembly, trace back to the tubing lot, then identify all other assemblies that used the same lot. Record elapsed time, gaps and quantity reconciliation. A supplier certificate cannot compensate for missing internal consumption records.

Parent-child lot control preserves traceability when a supplier reel is divided into cuts, kits and finished assemblies.
Control Supplier and Product Changes
Define changes that require notification or approval: resin source, formulation, additives, pigment, liner, dimensions, tooling, extrusion line, cross-linking method or site, expansion equipment, test method, print, packaging, subcontractor and manufacturing location. The required response may be document review, sample approval, partial testing or full requalification depending on risk.
The heat shrink manufacturer audit checklist supports factory and process review, while the RFQ specification checklist provides quotation fields.
Track supplier performance through accepted quantity, on-time delivery, shortages, lot rejection, production disruption, complaints, corrective-action timeliness and recurrence. Normalize metrics so a small supplier or short observation period is not compared misleadingly with a mature high-volume source.
React to Nonconforming Bulk Supply
Quarantine the affected lot and potentially related material. Confirm labels, records, dimensions and processing history before retesting. Define the affected scope using evidence rather than only the failed reel. Require containment, root cause, corrective action and effectiveness verification. A replacement shipment does not close the systemic cause.
Bulk Sourcing Release Checklist
Before issuing a production purchase order, confirm:
- The application, drawing and product revision are controlled.
- Fit uses maximum pass-over and minimum substrate tolerances.
- Material, wall, color, liner and print are defined.
- Required standards and evidence match the exact product scope.
- Production-intent samples and validation are approved.
- Reel/cut format, joints, length and labels are controlled.
- Incoming inspection, retention and reaction plans are assigned.
- Lot traceability works through cutting and assembly.
- MOQ, price breaks, freight, lead time and capacity assumptions are documented.
- Supplier changes require defined notice and approval.
- Deviations, owners and expiry dates are visible.
Work With TONFUL
Send TONFUL the application drawing, dimensions, material and construction, estimated volume, reel or cut format, testing evidence, packaging, labels and change-control requirements. TONFUL can discuss available bulk heat shrink tubing options and production-intent samples. Final MOQ, price, lead time, capacity, ratings and certification scope must be confirmed in the project quotation and controlled documents.
—