combination switch endurance testing must reproduce the electrical role, mechanical operation, and environmental conditions defined for the project. A cycle count alone proves little if the contact load, switching timing, actuator fixture, temperature, monitoring method, sample quantity, and failure criteria are missing. Direct-load contacts, relay requests, resistor-coded BCM inputs, illumination circuits, and momentary fog or dimmer controls may require different channels and acceptance logic.
TONFUL supplies automotive combination switch references for multiple vehicle applications. Confirm the exact vehicle, complete OE reference, connector, pinout, function matrix, control architecture, approved sample and project-specific validation plan before ordering or testing.
Quick Evidence Matrix

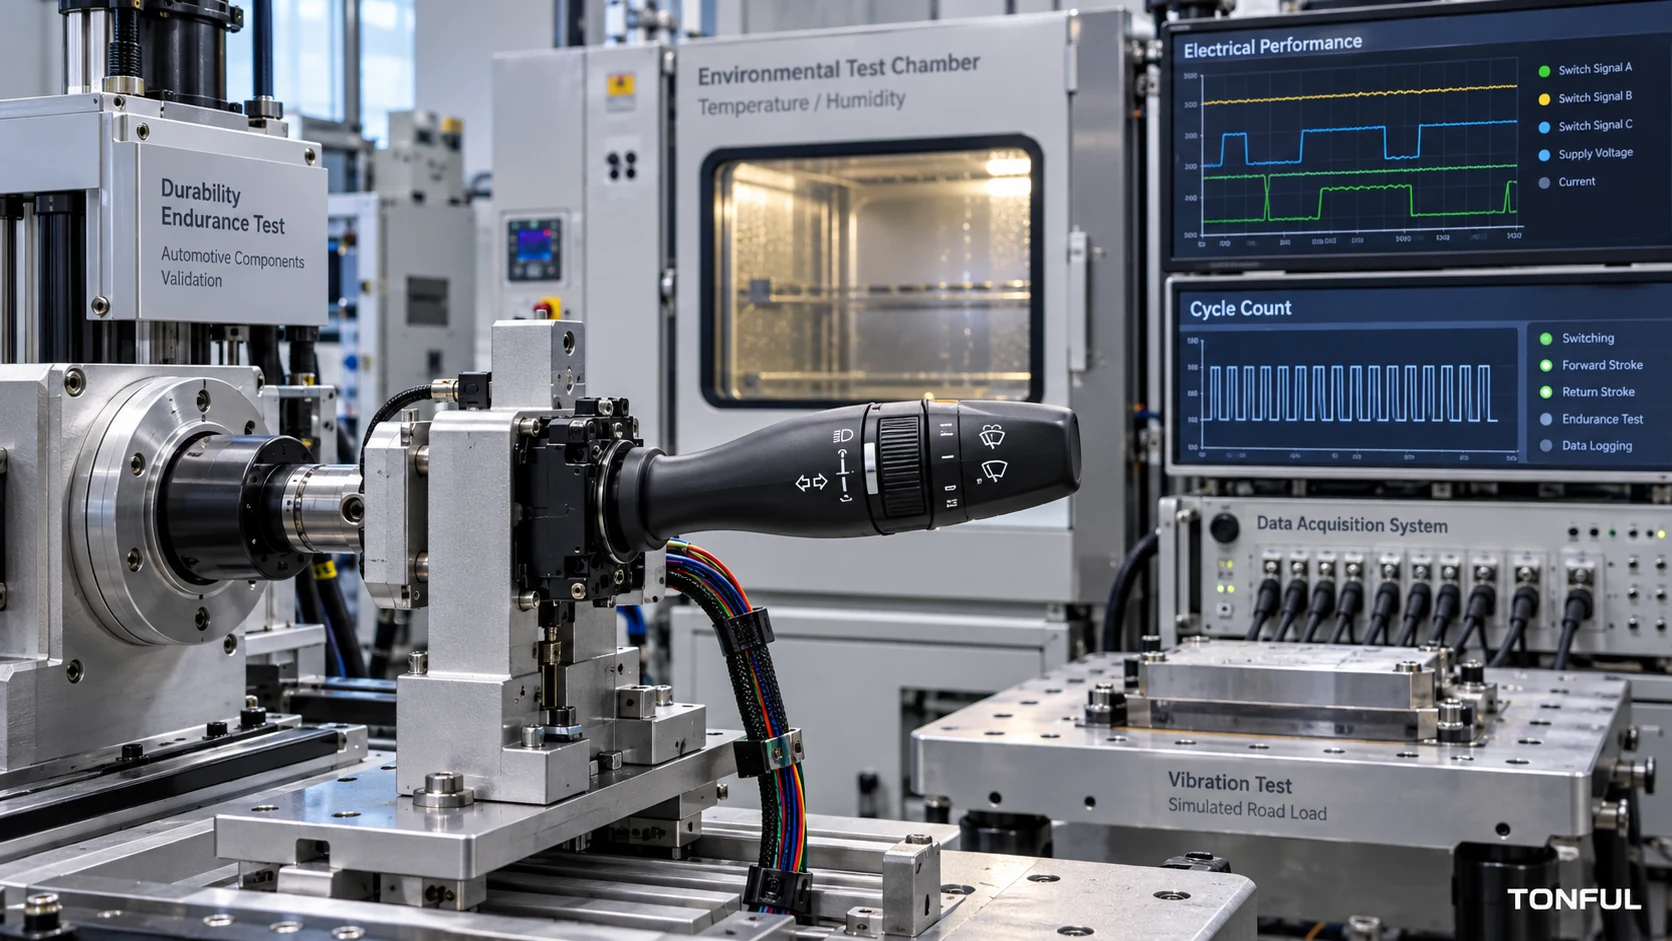
Conceptual illustration only – not a vehicle procedure, laboratory result, universal limit, or acceptance standard.
| Work area | Required focus | Acceptance source |
|---|---|---|
| Define the Test Object and Architecture | Freeze part number, revision, lot, vehicle application, connector, function matrix and whether each channel is direct-load, relay-controlled, ground-side, resistance-coded or module interpreted. | Project specification, approved plan, or root-cause evidence |
| Specify Electrical Loads for Every Channel | Document nominal and operating voltage, current or simulated input, load type, inrush behavior, polarity, suppression, switching phase, wiring resistance and protection. | Project specification, approved plan, or root-cause evidence |
| Define Mechanical Cycles and Actuation | State which turn-signal strokes, self-cancel actions, beam changes, wiper detents, washer pushes, cruise buttons and integrated functions form one sequence. | Project specification, approved plan, or root-cause evidence |
| Control Environment and Conditioning | Record temperature, humidity, vibration, dust, chemical exposure, thermal transitions and preconditioning only when required by the qualification plan. | Project specification, approved plan, or root-cause evidence |
| Monitor Degradation During the Test | Define inspection intervals and continuously or periodically monitor function, contact path, voltage drop, resistance, output state, actuation, illumination, temperature and abnormal events as appropriate. | Project specification, approved plan, or root-cause evidence |
| Set Failure Criteria Before Testing | Acceptance criteria must come from the product specification, customer requirement, approved drawing or qualification plan. | Project specification, approved plan, or root-cause evidence |
The matrix defines evidence categories, not pass values. Unknown requirements must remain open until the document owner confirms them.
For every section below, identify the applicable component, circuit and sample, then retain objective evidence. Any numeric requirement must cite the product drawing, OEM or customer specification, qualification plan or approved test procedure. This rule is stated once here; the section-specific records below address different technical risks.
Define the Test Object and Architecture
Freeze part number, revision, lot, vehicle application, connector, function matrix and whether each channel is direct-load, relay-controlled, ground-side, resistance-coded or module interpreted. Include mating connectors, terminals and harness interfaces when the qualification plan treats them as part of the test system.
Architecture determines what endurance is actually exercising. A direct-load switch may interrupt lamp current at its contacts, while a relay-controlled switch may operate only the relay coil. A BCM input can be a discrete state, a resistance-coded value or a momentary request interpreted by software. Testing all three with the same load would create evidence for the wrong design. Build a channel map that identifies power, ground, outputs, encoded inputs, illumination and communication-related pins, then tie every monitored state to the controlled circuit document.
Specify Electrical Loads for Every Channel
Document nominal and operating voltage, current or simulated input, load type, inrush behavior, polarity, suppression, switching phase, wiring resistance and protection. Use customer or OEM load profiles; do not substitute a generic lamp or relay because its steady current appears similar.
For a load-switching contact, the plan should distinguish make, carry and break conditions and identify whether the load is resistive, inductive, electronic or lamp-like. Inrush, inductive release and supply transients can stress contacts differently from steady current. For a low-level BCM input, the important evidence may instead be stable state voltage, resistance window or logic recognition throughout actuation. Record the actual load hardware or simulator revision, wiring impedance, protection and data-acquisition points so another laboratory can reproduce the circuit.
Define Mechanical Cycles and Actuation
State which turn-signal strokes, self-cancel actions, beam changes, wiper detents, washer pushes, cruise buttons and integrated functions form one sequence. Define cycle count, rate, dwell, actuator force or travel, alignment, rest periods and whether electrical switching occurs during movement. Avoid a fixture that side-loads the shaft or masks weak detents.
Describe one cycle as an explicit state sequence, for example OFF to parking lamps to controlled outputs and back, including any pull or push operations required by the project. State which contacts are energized at each transition. A cycle counter should advance only after the defined sequence is completed; retries, fixture stops and partial movements need separate event codes. Use position sensing or another suitable confirmation method when an actuator command alone cannot prove that the stalk reached the required detent.
Control Environment and Conditioning
Record temperature, humidity, vibration, dust, chemical exposure, thermal transitions and preconditioning only when required by the qualification plan. Identify whether endurance runs before, during or after each exposure. Do not assign universal severities from ISO 16750 without confirmed applicability.
Environmental sequencing matters. Electrical cycling during a climatic exposure can reveal behavior that a separate room-temperature check will not, while vibration before endurance may loosen an interface that later heats under load. The plan should therefore state sample allocation, exposure order, recovery time, conditioning state and whether the same samples continue into subsequent tests. Record chamber identity, sensor locations, actual profiles, interruptions and excursions rather than retaining only the programmed setpoints.
Sample Allocation
Define whether each test uses independent samples or a sequenced group, and retain an unaged reference sample when comparison is required. Allocate destructive-analysis samples before testing. The approved plan must name the authority and rationale for sample quantity, lot representation and selection. It must also state whether a failed sample may be replaced, whether completed results remain valid and how replacements are identified; an unplanned substitute cannot silently convert a failed sequence into a pass.
Monitor Degradation During the Test
Define inspection intervals and continuously or periodically monitor function, contact path, voltage drop, resistance, output state, actuation, illumination, temperature and abnormal events as appropriate. Preserve the first cycle and condition at which chatter, missed state, intermittent open, heat or mechanical damage appears.
Select monitoring by architecture. A direct-load path may need current, loaded voltage drop and temperature trending; a relay request may need coil-current or output-state confirmation; a resistance-coded input may need measured value and decoded state. Correlate electrical data with commanded position and cycle number. Sampling too slowly can miss contact bounce or intermittent opens, so the acquisition method and event threshold must be justified against the failure being sought.
Set Failure Criteria Before Testing
Acceptance criteria must come from the product specification, customer requirement, approved drawing or qualification plan. Address functional errors, electrical limits, unstable states, temperature evidence, mechanical damage, symbol or illumination failure, connector damage and post-test performance. Never create limits after seeing results.
Separate a test interruption from a product failure. Loss of chamber control, fixture misalignment, broken external wiring or acquisition failure may invalidate an interval without proving the switch failed. The approved procedure should define who can declare a test invalid, what evidence must be retained, whether completed cycles remain creditable and when replacement samples or retesting are allowed. A failed sample should not be repeatedly operated until its first-failure condition is lost.
Failure Evidence Matrix
Use the matrix below to connect an observed condition with evidence and containment. It is a diagnostic framework, not a list of universal rejection thresholds.
| Observed condition | Evidence to capture | Immediate action | Possible investigation path |
|---|---|---|---|
| Missed or incorrect switch state | Commanded position, decoded state, contact channel, cycle and timestamp | Pause according to the approved plan and preserve the state | Verify fixture travel, pin mapping, contact continuity, resistance-coded value and module interpretation |
| Intermittent open or contact chatter | High-speed voltage/current trace, actuator position and event duration | Protect the load and mark the first event | Repeat only as authorized; examine contact wear, spring force, contamination and terminal stability |
| Rising contact resistance or voltage drop | Initial, interim and final readings; test current; probe points; temperature | Review trend and affected channels | Confirm measurement system, isolate switch from connector losses and inspect contact surfaces |
| Abnormal temperature rise | Sensor location, ambient, load, current, voltage drop, thermal image and cycle | Stop at the safety threshold defined by the plan | Check contact resistance, terminal grip, connector fit, wiring impedance and excess load |
| Detent, return or actuator degradation | Force/travel trace, position repeatability, video and physical inspection | Prevent further cycling from erasing the condition | Inspect springs, cams, lubrication, shaft alignment, housing and fixture side load |
| Illumination or symbol failure | Supply condition, brightness/function result, visual record and cycle | Identify whether the fault affects safety or test continuation | Separate LED/lamp, resistor, solder, terminal and optical-component causes |
| housing, stalk or mounting damage | Setup photographs, crack or wear location, fixture loads and environment | Preserve parts without disassembly until review | Compare mounting geometry, actuator alignment, material condition and environmental sequence |
| Connector or terminal damage | Mating-cycle history, terminal position, retention evidence, heat marks and harness support | Quarantine the sample and mating interface | Inspect terminal engagement, retention, plating, strain, contamination and connector compatibility |
Test or Investigation Record

This conceptual record layout supports traceability; it does not replace the controlled test or investigation form.
Use a vertical record that remains readable on mobile screens and can be transferred into a laboratory form:
| Record field | Required entry |
|---|---|
| Sample identity | Part number, revision, manufacturing lot, sample ID, build status and approved deviation |
| Application and channel | Vehicle or project, connector, pin, function and control architecture |
| Electrical load | Voltage, current or signal, load type, inrush or release condition, protection and wiring impedance |
| Cycle sequence | Switch actions, energized state, rate, dwell, planned cycles and completed count |
| Fixture and environment | Actuator-tool revision, orientation, conditioning, exposure sequence and actual chamber profile |
| Monitoring | Equipment ID, range, accuracy, calibration status, and probe or sensor locations |
| Results | Initial, interim and final measured values with raw-data reference |
| Failure | First failure cycle, test condition, symptom, immediate containment and preserved evidence |
| Validity and retest | Interruption or invalid-test reason, disposition, approving authority and retest scope |
| Approval | Acceptance-source document and clause, pass/fail, reviewer and date |
For example, an electrical-load entry should identify the approved load profile rather than say only “lamp,” and a failure entry should record the first affected cycle and evidence file rather than only “failed.” Define sample quantity, equipment suitability, invalid-test rules, retest authority and data retention before execution. A summary pass/fail field cannot replace raw readings and photographs.
The official ISO pages describe distinct environmental-load categories for road-vehicle electrical and electronic equipment: ISO 16750-2:2023 covers electrical loads, ISO 16750-3:2023 covers mechanical loads, and ISO 16750-4:2023 covers climatic loads. Apply a part only when the project or customer specification selects it, then confirm the applicable edition, mounting location, method, severity, sequence and acceptance source. These standards do not by themselves establish a universal combination-switch cycle count, contact-resistance limit, vibration severity, temperature limit or release criterion.
ISO 16750-2 addresses electrical loads but explicitly excludes electromagnetic compatibility. If the switch contains electronics, encoded outputs, communication interfaces or module-interpreted signals, define separate customer-approved EMC and ESD requirements. Component testing alone does not establish completed-vehicle EMC compliance; record the applicable configuration, harness, operating mode, test plan and acceptance source.
Internal Links and Decision Path
Use TONFUL’s product range, contact-resistance method, failure guide, OE-reference guide and truck selection checklist as the linked path from application identity to testing and release.
Supplier, Release, and Change Control
For an RFQ or validation request, provide the vehicle, OE chain, connector, function matrix, architecture, load definition, environment, sample quantity, test plan and acceptance sources. Request controlled drawings, raw-data references, nonconformance handling and change notification.
Receiving inspection should compare lot identity, housing, connector, terminals and functions with the approved sample. Define reaction plans for discrepancies and changes that may require notice or reapproval.
Final Release Checklist
- Scope, application, part revision, sample quantity and lot are identified.
- Electrical architecture, functions, loads, environment and conditions are documented.
- Equipment, fixtures, probes, ranges, accuracy and calibration status are recorded.
- Actual results, failure modes, photographs and raw-data references are retained.
- Every limit points to an approved source; no universal value is invented.
- Invalid tests, retests, deviations and unresolved items have documented disposition.
- Approved sample, receiving controls, traceability and change notification are defined.
- Release identifies reviewer, date, approved scope and closure evidence.
Planning, Evidence Review, and Test Purpose
Before Execution
Before execution, confirm channel coverage, fixture validity, safety controls, acquisition versions and acceptance sources. Resolve document conflicts before testing.
After Testing
A reviewer must reconstruct the decision from sample identity, setup, calibration, readings, event logs and source clauses. Assign open items an owner, due date and closure evidence.
Qualification vs Audit vs Production Monitoring
Qualification tests defined samples; audits examine process controls; production monitoring tracks selected characteristics. State each activity’s purpose, sample source, reaction plan and authority.
Preserve failed samples and separate design, process, fixture, load and setup causes. Relevant product or process changes require risk review and possible regression testing or reapproval.
Work With TONFUL
Send TONFUL the complete application and evidence package rather than only a switch photograph or symptom. TONFUL can compare the request with current combination-switch applications and OE references, then align sample review and project-specific validation requirements. Final approval remains tied to controlled documentation, agreed tests and the approved sample.