
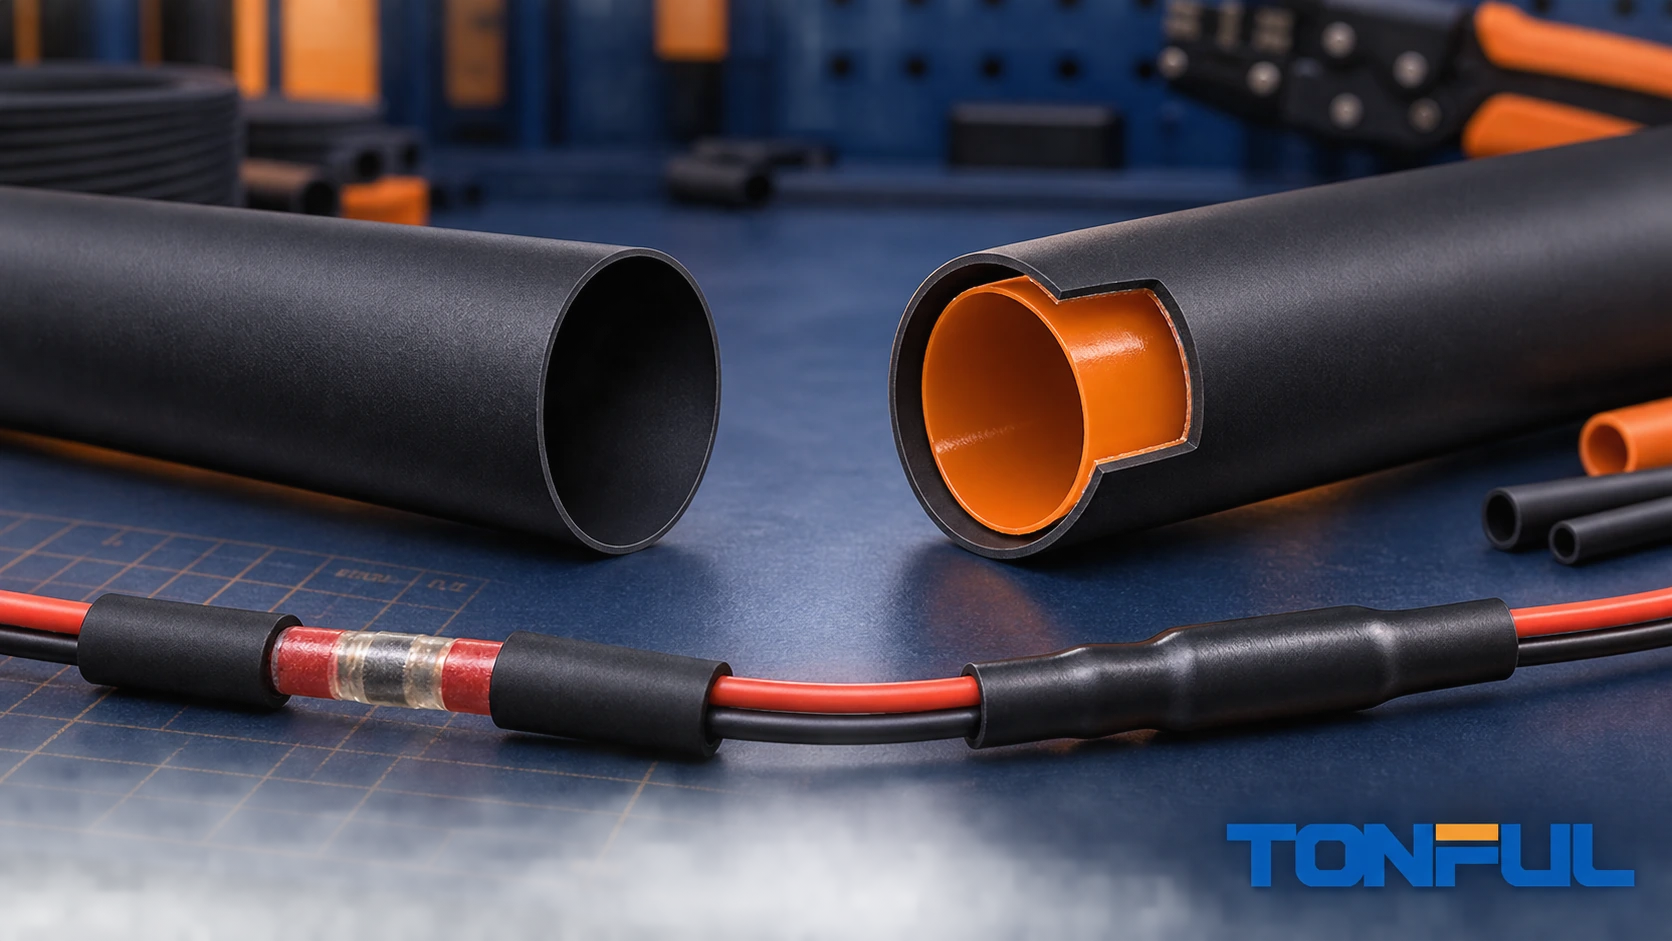
Single-wall and dual-wall heat shrink tubing can share the same outside appearance before installation, yet they perform different jobs. Single-wall tubing consists of one recoverable polymer layer. Dual-wall tubing adds an internal adhesive or sealant that softens during heating while the outer layer recovers. The second layer can improve environmental protection and strain transition, but it also changes sizing, heating, inspection, stiffness, rework and cost.
This comparison helps engineers and buyers decide which construction fits the assembly. It does not assign universal temperature, voltage, IP or flame ratings. Those properties must be verified for the exact material, series, size, color and completed application.
On this page: Construction | Selection matrix | Sealing | Sizing | Process | Approval
How the Constructions Differ
Single-Wall Construction
Single-wall tubing has one recoverable polymer wall. Depending on the product family, it may be thin, flexible, semi-rigid, transparent, colored, printable or made from a specialty polymer. It is frequently evaluated for electrical insulation, color coding, wire identification, light abrasion protection, component covering and strain transition.
Because there is no separate flowable liner, the tube mainly conforms through radial recovery. It can grip a reasonably uniform substrate, but it does not normally fill valleys between conductors or steps around a splice. Close visual contact at the ends should not be described as a verified environmental seal.
Dual-Wall Construction
Dual-wall tubing combines a recoverable outer wall with an inner adhesive or sealant. During controlled heating, the outer layer shrinks while the liner softens and flows toward gaps and substrate surfaces. The construction is often considered for splice protection, connector backshell transitions, cable ends and outdoor, automotive or marine assemblies.
The two layers must be specified separately. The outer polymer controls much of the mechanical and environmental behavior; the liner influences bonding, gap filling and sealing. “Dual wall” does not identify the adhesive chemistry, compatible substrates, shrink ratio, recovered wall or test evidence.
The TONFUL heat shrink tubing product page can be used to discuss available constructions, but final selection requires a model-level drawing and supporting records.

Conceptual illustration only—not an acceptance standard or laboratory cross-section.
Single-Wall vs Dual-Wall Comparison
| Decision factor | Single-wall tubing | Dual-wall adhesive-lined tubing | Required verification |
|---|---|---|---|
| Construction | One recoverable polymer layer | Recoverable outer wall plus adhesive or sealant | Cross-section, drawing and material identity |
| Primary role | Insulation, identification, compact protection | Environmental protection, gap filling and strain transition | Application function and failure consequences |
| Installed profile | Usually lower and more flexible for comparable family | Often thicker or stiffer after recovery | Recovered wall and bend study |
| Irregular geometry | Conforms but does not intentionally fill internal valleys | Liner may flow into compatible gaps | Sectioning or specified assembly test |
| Heating | Generally lower thermal mass | Must recover outer wall and activate liner | Equipment, sequence, component temperature and endpoint |
| Inspection | Position, recovery and surface defects | Adds adhesive flow, void and end-seal observations | Defined visual criteria correlated to validation |
| Rework | Usually easier to cut away carefully | Adhesive can bond to substrate and complicate removal | Approved rework method and damage inspection |
| Supply cost | Often lower for comparable basic product | Added liner and process can increase cost | Accepted installed cost, not unit price alone |
This table compares construction, not performance grades. A specialty single-wall fluoropolymer can cost more and tolerate a different environment than a general-purpose dual-wall polyolefin product.

The corrected matrix avoids universal seal or heat settings and identifies the evidence required for each decision.
When Single-Wall Is Usually the Better Starting Point
Single-wall tubing is a logical first candidate when the assembly needs compact insulation, color identification, printed marking or abrasion protection without a defined environmental seal. It is also useful when flexibility, low weight, rapid heating or easier rework matters.
Typical evaluation cases include uniform wire sections, component leads, control-panel identification, harness color coding and protected indoor assemblies. The candidate still needs adequate expanded ID, recovered ID, wall and temperature evidence. If moisture can reach a conductive joint through the tube ends, single-wall tubing should not be credited with blocking that path unless the assembly has another verified seal.
The types of heat shrink tubing guide explains how single-wall construction combines with material, ratio, thickness and identification functions.
When Dual-Wall Is Usually the Better Starting Point
Dual-wall tubing is considered when the interface needs adhesive-assisted sealing, additional strain transition or improved resistance to movement around an irregular splice or cable end. It can be useful where the joint sees splash, condensation, salt, dirt or outdoor exposure, provided the selected liner is compatible and the completed assembly passes the required test.
It may also help when one tube must bridge a splice barrel and smaller wire insulation. However, a large geometry transition may require 3:1 or 4:1 dimensions; dual-wall construction alone does not create a high shrink ratio. Use the heat shrink ratio guide and exact size table together.
Do not choose dual wall merely because it sounds more durable. In a sealed enclosure with no moisture requirement, the adhesive may add cost, cycle time and rework difficulty without project value. On silicone, fluoropolymer or contaminated substrates, the liner may not bond as expected.
What Dual-Wall Sealing Can and Cannot Prove
Adhesive Flow Is Not Automatically an IP Rating
An adhesive bead at both ends shows that liner movement occurred at visible locations. It does not reveal every internal void, wetting condition or capillary path. IP ratings apply to tested enclosures or interfaces under defined configurations and methods. A tubing catalog claim cannot be transferred to any wire, connector, cut length and heating process.
For a critical seal, identify the tested assembly, substrate, tubing size, overlap, preparation, conditioning and acceptance method. Depending on the project, validation may include leakage, immersion, pressure cycling, humidity, salt exposure or electrical measurements before and after conditioning. Do not invent a universal test.
Substrate Compatibility Matters
Adhesive may wet PVC, cross-linked polyolefin, metal, painted surfaces or engineering plastics differently. Mold release, oil, oxidation, moisture and handling contamination can reduce bonding. Some low-surface-energy materials need a product-specific adhesive or preparation.
Use production substrates and approved cleaners in development. Do not substitute aggressive solvents without confirming compatibility with wire insulation, seals, markings and the liner. Record the cleaning and handling method in the work instruction.
The marine heat shrink tubing guide illustrates why salt, moisture and corrosion must be treated as completed-assembly requirements rather than marketing labels.
Size Each Construction From Its Own Drawing
Both constructions need a minimum expanded ID that clears the largest feature and a maximum recovered ID below the smallest required substrate. Dual-wall tubing also needs enough recovery pressure and liner volume for the intended interface without excessive adhesive displacement.
Do not compare nominal sizes across constructions as though they are identical. A dual-wall product can have different recovered wall, stiffness and dimensional tolerances from a single-wall product with the same nominal diameter. For a connector-to-cable transition, record:
- Largest pass-over diameter or controlling perimeter.
- Minimum cable or bundle diameter.
- Installation clearance established by trial.
- Expanded ID minimum and recovered ID maximum.
- Outer, adhesive and total recovered wall where specified.
- Longitudinal-change limit and required final coverage.
The heat shrink tubing size guide provides the two-boundary calculation and cut-length method.
Installation and Inspection
Heating Single-Wall Tubing
Use controlled hot air, an oven or another qualified process compatible with the product and assembly. Heat evenly and inspect for complete recovery, position, wrinkles, splits, scorching, holes and movement. A lower heat-source setting does not prove the polymer reached full recovery, while a high setting can damage the surface before the full circumference heats.
Heating Dual-Wall Tubing
The process must recover the outer wall and activate the liner without overheating nearby insulation, seals or connectors. Metal splice barrels can draw heat away. Long sleeves can trap air or push adhesive unevenly if the heating sequence is uncontrolled. Define where heating starts, how it moves and what endpoint operators use.
Inspect visible adhesive flow, but connect that criterion to development evidence. For high-risk joints, section selected samples during qualification to review internal coverage. Clearly label conceptual diagrams; they are not laboratory cross-sections or acceptance standards.
Rework Boundaries
De-energize and follow the assembly’s service procedure. Cut tubing with tools and depth controls that protect the conductor, insulation, terminal plating and connector. Adhesive residue may hide damage or alter the surface for a replacement seal. Define whether rework is permitted, how the substrate is cleaned and what reinspection or retest is required.

Validate both recovery processes on the complete assembly; no universal heat setting is implied.
Compare Accepted Installed Cost
Single-wall tubing may reduce material cost and heating time. Dual-wall tubing may eliminate a separate sealant or improve environmental protection, but it can add cutting, heating, inspection and rework costs. Compare the total accepted assembly:
Installed cost = tubing + cutting + preparation + heating + inspection + scrap + rework + validation allocation
Do not count the same waste or labor twice. Include storage and shelf-life control where the adhesive has documented limits. For bulk sourcing, the bulk heat shrink tubing guide covers packaging, lot traceability and supplier changes.
Validation and Release Record
| Record field | Required entry |
|---|---|
| Assembly | Drawing, revision, substrate materials and tolerance range |
| Tubing | Manufacturer, part number, material, wall construction, adhesive and color |
| Dimensions | Expanded/recovered ID, wall, ratio and longitudinal change |
| Process | Equipment, fixture, heat sequence, endpoint and parameter limits |
| Visual inspection | Position, recovery, damage, adhesive flow and permitted defects |
| Qualification | Sample allocation, conditioning, test method and acceptance source |
| Rework | Permission, removal method, substrate inspection and retest |
| Decision | Approved scope, deviations, owner, reviewer and date |
UL Solutions explains that its insulating tubing certification program covers submitted tubing products with different polymer and construction features, including heat-shrinkable products and meltable liners. Verify the exact recognized product and conditions; do not treat dual-wall construction as a certification.
Discuss Wall Construction With TONFUL
Send TONFUL the application, largest and smallest diameters, substrates, moisture or sealing requirement, material preference, temperature and fluids, required evidence, cut length, packaging and volume. TONFUL can discuss single- and dual-wall candidates within its documented supply range. Final release should remain tied to the exact product and validated assembly process.