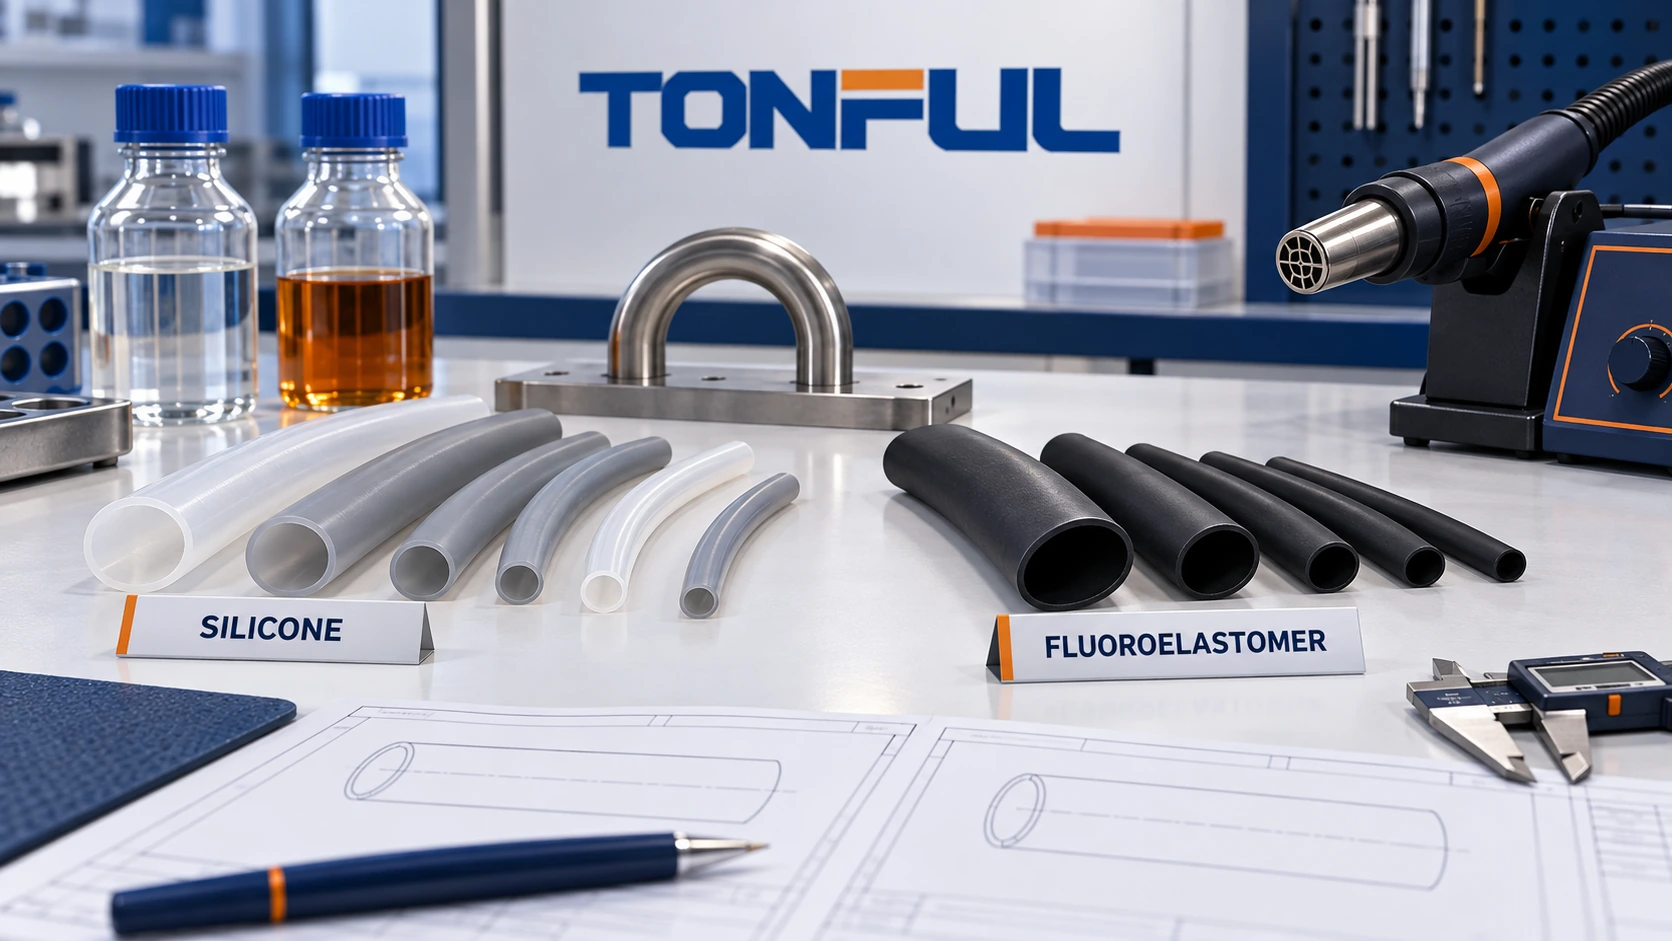
Silicone and fluoroelastomer heat shrink tubing can both serve demanding harnesses, but their strengths are not interchangeable. Silicone products are often considered where flexibility across a broad temperature range matters. Fluoroelastomer products are commonly evaluated where hot oils, fuels, hydraulic fluids or aggressive service conditions drive the specification. Those tendencies are useful for screening, not for approving a part.
The correct choice depends on the exact formulation, tubing construction, recovered dimensions, installation process and qualification evidence. A material family name does not establish fluid compatibility, flame behavior, temperature range, electrical rating or aerospace approval. This guide shows engineers and buyers how to compare production-intent silicone and fluoroelastomer tubing without inventing universal limits.
Quick Comparison
| Decision area | Silicone heat shrink tubing | Fluoroelastomer heat shrink tubing | Evidence to request |
|---|---|---|---|
| Primary selection driver | Very high flexibility and low-temperature movement are common reasons for evaluation | Hot-fluid, fuel and chemical exposure are common reasons for evaluation | Exact product data sheet and project exposure list |
| Mechanical feel | Often soft and compliant | Often firmer and more abrasion-oriented | Recovered sample bend, abrasion and cut-through results |
| Installation | Recovery conditions vary by formulation and size | Recovery may require substantial controlled heat | Approved time-temperature process and substrate limit |
| Fluids | Must be checked against each fluid and concentration | Often selected for fuel, oil or hydraulic-fluid resistance | Product-specific immersion method and retained properties |
| Electrical use | Insulation performance must be tied to size, wall and condition | Same requirement; material name alone is insufficient | Test method, specimen and assembly requirement |
| Compliance | Claims vary by product, color and size | Claims vary by product, color and size | Current report, file, specification and scope |

Use the material family to narrow candidates, then compare the exact products under the same controlled conditions.
Start With Product Construction
“Silicone” may describe different silicone-rubber formulations, crosslinking systems, pigments and wall designs. “Fluoroelastomer” can describe multiple fluorinated elastomer formulations, including products commonly associated with FKM-type chemistry. Suppliers may modify compounds to balance heat resistance, flexibility, fluid behavior, flame performance and processing. Two products with the same broad material label can therefore behave differently.
Record the manufacturer, product family, part number, revision, color, size, expanded inside diameter, maximum recovered inside diameter, recovered wall and supplied form. Confirm whether dimensions are minimum, maximum or nominal. If a project requires a controlled material specification, retain the compound or specification reference permitted by the supplier rather than relying on a catalog category.
The broader heat shrink tubing material guide helps compare these elastomers with polyolefin, PVC and fluoropolymer alternatives. Do not assume that silicone heat shrink is the same as extruded silicone sleeving or that a fluoroelastomer tube is the same as PTFE, FEP or PVDF tubing.
Flexibility, Bend Radius and Harness Movement
Silicone heat shrink is frequently evaluated for flexible harness sections, sensor leads and assemblies that must remain compliant at low temperature. However, “flexible” needs a test condition. A room-temperature hand bend does not predict stiffness after thermal aging, fluid exposure or repeated movement. Specify the assembly temperature, bend radius, cycle count, mandrel geometry and post-test inspection or electrical checks.
Fluoroelastomer tubing may offer a different balance of flexibility, toughness and abrasion behavior. A firmer recovered jacket can support rugged harnessing, but it may also concentrate stress at a transition if overlap, wall or routing is poorly designed. Compare both candidates on the actual cable, braid, splice or backshell geometry.
Check recovered fit, wrinkles, wall uniformity, longitudinal change, edge lifting and movement at the transition. If the tube forms strain relief, define the permitted flex zone and verify that the protected conductor does not bend sharply at the sleeve edge. The heat shrink tubing size guide explains pass-over and recovered-fit calculations, but final dimensions must come from the quoted product data.
Temperature Means More Than One Number
Keep four thermal concepts separate: storage range, installation or recovery conditions, continuous operating range and short-duration exposure. A product may tolerate a high service temperature yet require an installation process that damages the wire insulation, connector seal, solder joint, adhesive, sensor or nearby polymer. Conversely, a compliant low-temperature installation does not prove long-term service performance.
Create a thermal budget for the completed assembly. Record nozzle or oven set point, measured part temperature where practical, heating time, distance, airflow, fixture, rotation and cooling. Evaluate the coldest and hottest process locations. For thick or irregular assemblies, surface temperature alone may not show whether the wall has fully recovered.
TE Connectivity’s official harnessing tubing overview lists separate silicone and high-temperature fluoroelastomer product families with product-specific operating ranges and specification references. It is useful evidence that formulations differ; it does not authorize applying one listed range or qualification to another supplier’s tubing.
Fluid and Chemical Compatibility
Fluid resistance is often the decisive difference. Build an exposure list from the real location: fuel, engine or transmission oil, hydraulic fluid, coolant, cleaning agents, deicing fluid, lubricants, salt solution, water, ozone and process chemicals. Include concentration, temperature, duration, splash or immersion, pressure, drying and repeated exposure. Trade names alone are insufficient when formulations change.
Fluoroelastomer tubing is commonly screened for hot-oil, fuel and hydraulic-fluid environments, while silicone may be selected for flexibility and temperature behavior. Neither statement is an acceptance criterion. Some fluids can swell, soften, embrittle, discolor or extract additives from an elastomer. The substrate and any adhesive, label or ink may fail before the outer tubing.
Measure the properties that matter after conditioning: mass or dimension change, tensile behavior, elongation, hardness, cracking, adhesion, dielectric performance and assembly function. Use unaged controls from the same lot. A visual “no damage” result cannot replace the specified retained-property requirement.

Fluid testing should reproduce the project medium, temperature, exposure mode and post-conditioning acceptance method.
Abrasion, Tear and Installation Damage
Soft tubing is not automatically weak, and a firmer product is not automatically abrasion-proof. Compare recovered wall, surface friction, tear propagation, edge condition and resistance to the actual contact surfaces. A braided harness rubbing against a bracket creates a different challenge from a stationary sensor lead protected from handling.
Inspect installation damage separately from service damage. Excess heat, a sharp fixture, contaminated gloves or dragging expanded tubing over a burr can create cuts before the assembly enters service. Document the pass-over path and protect connector threads, braid ends and metal edges. If lubricant is permitted, identify it and verify compatibility; do not introduce an uncontrolled substance merely to ease installation.
For an application-specific test, state abrasive material, load, stroke, speed, cycle count, temperature and endpoint. For cut-through or pinch testing, define the fixture and force. Do not publish a universal minimum value unless the controlled drawing, customer specification or exact product qualification supplies it.
Electrical, Flame, Smoke and Outgassing Evidence
For electrical insulation, define operating voltage, transient exposure, creepage or clearance context, recovered wall, conductor geometry, temperature, contamination and test method. Dielectric strength measured on flat or standard specimens is not automatically an assembly voltage rating. Evaluate the finished joint if the tubing is part of the insulation system.
Flame retardancy, low smoke, low toxicity, halogen content and outgassing are separate claims. Silicone is not automatically low-smoke or approved for aerospace use. Fluoroelastomer is not automatically flame qualified for every platform. Record the test method, edition, classification, specimen condition, exact product scope and issuing document.
If outgassing or contamination is critical, define the required test and limits for the intended environment. The supplier’s generic material description cannot prove suitability near optics, electronics, clean processes or occupied spaces. RoHS and REACH declarations address regulated substances; they do not prove fire, electrical or mechanical performance.
Installation Process and Production Control
High-performance elastomeric tubing deserves a validated process, not operator judgment alone. Use the heat gun, oven and infrared process guide to choose a controllable heating method. Establish work instructions from approved trials with production-intent parts.
Record tubing lot, cut length, substrate, ambient condition, equipment ID, set point, verified part temperature if required, heating time, fixture, operator and final result. Confirm full recovery without scorching, gloss change, bubbles, splits, trapped air or damage to the underlying assembly. Measure longitudinal movement where sleeve position is critical.
For production monitoring, define start-up approval, changeover checks, sample frequency, reaction plan and revalidation triggers. Material, pigment, size, wall, supplier, equipment, tooling or process changes may affect performance. Receiving inspection should verify labeling, dimensions, appearance, lot traceability and required documents before material reaches the line.

A controlled process links incoming identity, heat application and final inspection to the approved assembly record.
Build a Comparable Validation Plan
Use production-intent samples and the same substrate geometry for both candidates. Keep an unaged control group. Decide whether environmental tests use independent samples or a defined sequence; a sequence can reveal interactions but may hide the cause of failure. Allocate separate samples for destructive tests and document replacement-sample rules before testing begins.
| Test area | Controlled inputs | Result and acceptance source |
|---|---|---|
| Identity and dimensions | Product, lot, color, expanded and recovered dimensions | Drawing or approved specification |
| Installation | Equipment, time, temperature, fixture and substrate | Approved process window |
| Thermal | Operating, storage, cycling or short exposure | Customer plan or product specification |
| Fluid | Medium, concentration, temperature, duration and drying | Retained-property requirement |
| Mechanical | Bend, abrasion, tear, cut-through or flex conditions | Drawing or qualification plan |
| Electrical | Test points, voltage/current method, conditioning | Controlled electrical requirement |
| Fire or special environment | Exact method, specimen and conditioning | Contract or program requirement |

The same controlled inputs and acceptance sources make candidate results comparable and auditable.
The heat shrink tubing testing guide provides a broader framework for sample identity, conditioning, dimensional records and failure evidence. Do not average away a critical defect. Preserve failed samples, images, raw data and lot information for root-cause review.
Which Material Should You Choose?
Consider a verified silicone product when very high flexibility, low-temperature movement or a soft transition is central and the exact product meets every fluid, mechanical, electrical and fire requirement. Consider a verified fluoroelastomer product when hot fuels, oils or hydraulic fluids dominate and the candidate also satisfies flexibility, installation and qualification needs.
Choose neither when the substrate cannot tolerate the recovery process, when the required seal needs an adhesive-lined construction unavailable in the selected family, or when another material has stronger project evidence. The lowest unit price is not necessarily the lowest installed cost. Include process time, scrap, inspection, rework, qualification, storage life, minimum order and continuity of supply.
Use the heat shrink tubing RFQ checklist to send suppliers the same requirement set. A quotation should identify assumptions and deviations rather than silently selecting a convenient product.
Work With TONFUL
Send TONFUL the substrate dimensions, pass-over geometry, operating and installation temperatures, fluid list, flex and abrasion conditions, electrical needs, required specifications, color, printing, annual volume and validation plan. TONFUL can discuss available silicone and fluoroelastomer heat shrink options and production-intent samples. Confirm all ratings, declarations and approval scope for the exact quoted product before release.
—