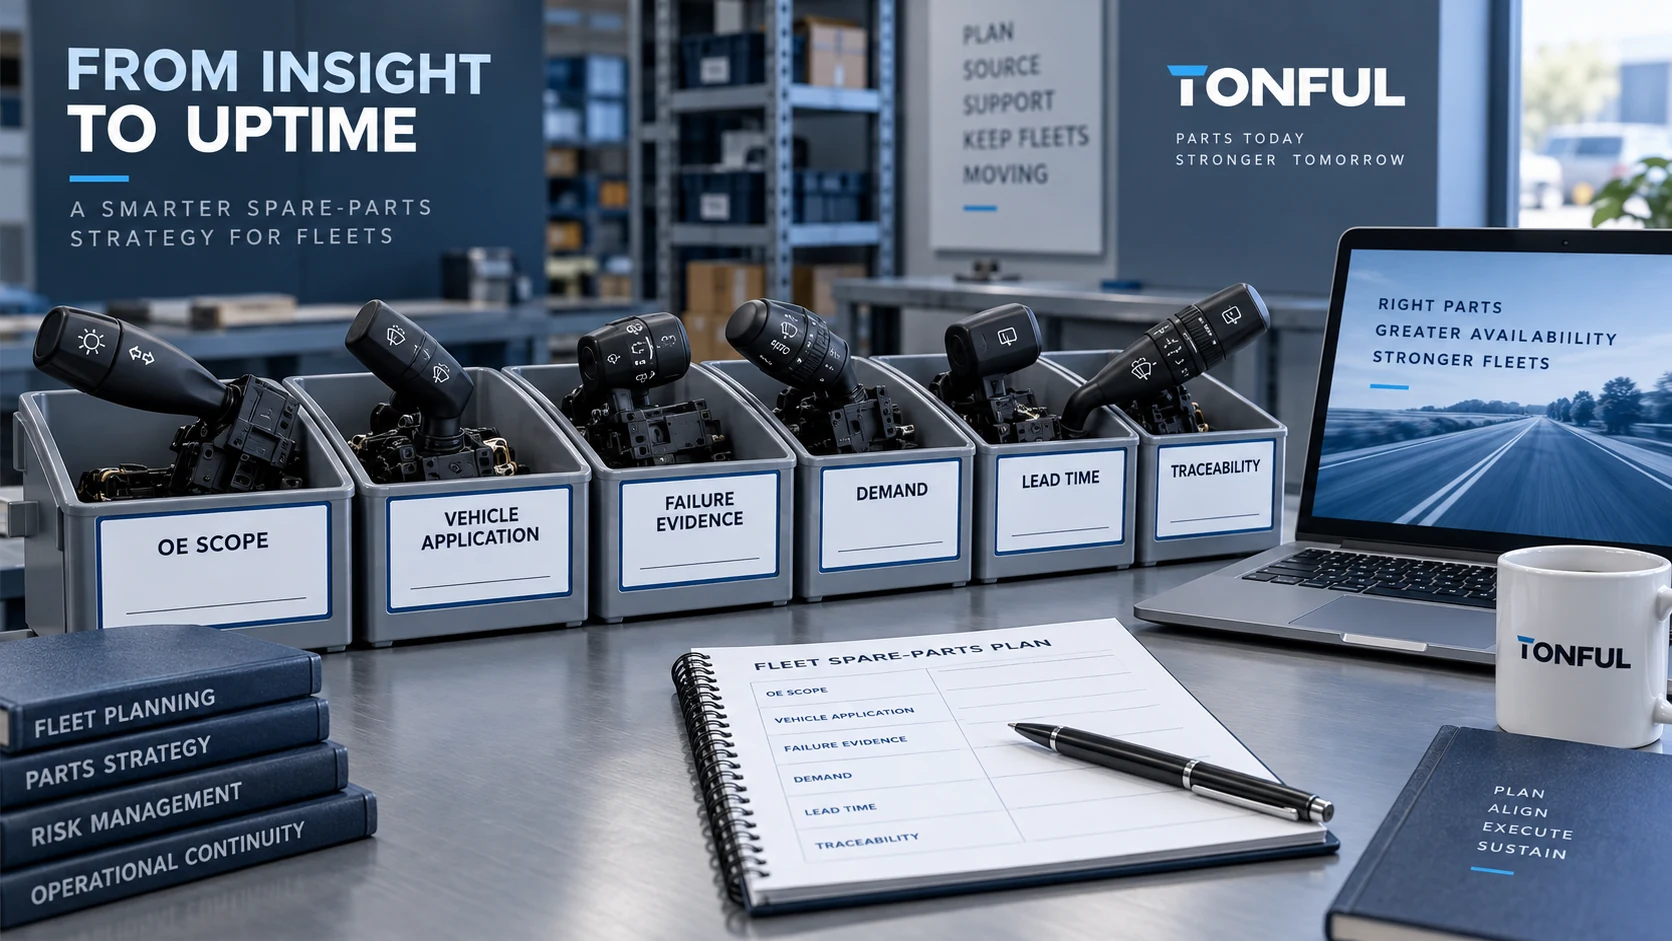
A fleet should not stock combination switches by connector appearance, truck brand or a single historical purchase number. The useful stocking unit is a verified application group: controlled OE and supersession references, vehicle configuration, switch architecture, function package and approved replacement evidence linked to observed demand.
Failure history matters, but replacement demand is not identical to switch failure. A no-wiper complaint may be caused by a fuse, wiring, motor, park circuit, controller or connector. Counting every issued switch as a failed switch inflates demand and hides diagnostic waste. A reliable plan connects part identity, confirmed failure mode, lead time, service criticality and traceability.
On this page: Build the Part Master | Convert Failures into Demand | Set Stocking Parameters | Control Inventory Risk
Build the Part Master
Control OE Numbers and Application Boundaries
Record the complete OE service number, suffix and supersession direction. Distinguish it from supplier numbers, engineering numbers, molded housing marks and distributor SKUs. Link each approved number to make/model, market, production or VIN/chassis boundary, steering side, cab/body, connector population, architecture and function package.
Use the combination-switch OE cross-reference guide to assign Verified, Conditional or Unverified status. Do not merge bins because two switches share a connector. The same-connector interchangeability guide explains why pinout, coded values, network software and options can differ behind the same shell.
| Master-data field | Required entry |
|---|---|
| Internal stock ID | Unique controlled inventory identifier |
| OE reference chain | Current number, prior number and replacement direction |
| Supplier/manufacturer number | Exact orderable number and revision |
| Vehicle scope | Market, model, production/VIN boundary, steering and cab/body |
| Architecture | Direct, relay, coded, LIN/CAN or documented combination |
| Function package | Lighting, turn, wiper, washer, cruise and optional controls |
| Connector definition | Shell, keying, cavity population and pinout revision |
| Approval evidence | Document/sample/vehicle record, approver and date |
| Traceability level | Lot, serial or receiving identity retained |
| Lead-time source | Supplier quote/order history and last update |
| Status | Active, conditional, blocked, superseded or obsolete |
Keep Traceability with the Part
The GS1 Global Traceability Standard distinguishes class-, batch/lot- and instance-level identification. It is a general traceability framework, not a combination-switch specification. Fleets can apply the principle by retaining the orderable part identity plus supplier lot or serial data when risk and available marking justify it.
At receiving, preserve label, lot, quantity, supplier, receipt date and purchase order. Avoid moving visually similar switches into an unmarked shared bin. If a field issue emerges, traceability should identify which vehicles received the affected lot without quarantining every switch in the fleet.

A controlled part master prevents visually similar but electrically different switches from sharing one stock record.
Convert Failures into Demand
Separate Complaint, Root Cause and Replacement
Create a closed maintenance record for each event. Record vehicle, mileage/hours, date, symptom, diagnostic evidence, confirmed root cause, installed part, removed-part disposition and whether the repair solved the complaint. The combination-switch diagnostic guide supports fault isolation before replacement.
| Complaint or finding | Possible cause outside the switch | Stock-planning treatment |
|---|---|---|
| No turn signals | Fuse, flasher/module, wiring, ground or lamps | Count switch demand only after switch fault is confirmed |
| Wipers do not run | Motor, relay/module, park circuit, harness or protection | Keep diagnosis separate from switch issue quantity |
| Intermittent operation | Terminal fit, connector heating, harness strain or contacts | Record evidence and the replaced component |
| Stalk will not cancel/return | Column/cancel interface, trim interference or switch mechanism | Confirm mechanical source and vehicle configuration |
| One optional button fails | Wrong variant, coded input, software or internal contact | Review application master before increasing stock |
| Thermal damage | High contact resistance, loose terminal or excessive load | Quarantine evidence and investigate system path |
| Replacement does not fix complaint | Misdiagnosis, wrong part or downstream fault | Do not count as validated switch consumption |
Classify failure modes consistently: electrical contact/open, voltage drop/heating, mechanical detent/return, symbol/illumination, connector/terminal, electronic/network, contamination/environment, wrong application and no-fault-found. The categories should be specific enough to reveal action but stable enough for trend analysis.
Define a Fair Observation Window
For each approved stock ID, state the installation start date, data cutoff, minimum service exposure and treatment of recently installed parts that have not completed the observation period. Separate regions, duty cycles or vehicle groups when their exposure is not comparable. Define whether repeated workshop visits count as service events, unique failed switches or unresolved complaints.
Do not publish a percentage without numerator, denominator and time basis. Useful measures include confirmed switch failures per vehicle-year, issues per installed replacement cohort and no-fault-found share. Keep warranty returns and workshop issues linked so the same event is not counted twice.
Translate History into Planning Inputs
Use issued quantity only after correcting known misdiagnosis, one-time campaigns, fleet expansion, cannibalization and returns to stock. Note seasonality where wiper or lighting usage changes demand. For a new vehicle family, use analogous history cautiously and label the assumption; update it as fleet evidence accumulates.
Criticality is separate from frequency. A rarely used switch can deserve stock when its failure immobilizes a vehicle, affects required lighting/wiping functions and has a long or uncertain lead time. A frequent but locally available item may need less safety stock.
Set Stocking Parameters
Segment by Demand, Criticality and Supply Risk
Use a simple portfolio rather than one rule for all parts:
| Segment | Typical evidence | Planning response |
|---|---|---|
| High demand / high criticality | Repeated confirmed use, downtime impact, stable application | Active local stock and frequent review |
| Low demand / high criticality | Rare use but immobilizing function or long recovery | Risk-based contingency quantity or shared pool |
| High demand / lower criticality | Predictable use and alternatives available | Replenishment based on measured demand/lead time |
| Low demand / lower criticality | Sparse consumption, short supply path | Central stock or order on demand |
| Unverified application | Cross-reference or vehicle approval incomplete | Quarantine from normal issue until verified |
| Obsolete/superseded | Fleet population declining or number replaced | Controlled run-down and transition plan |
NIST’s supply-chain guidance recommends mapping and assessing supply risk and considering alternatives or safety stock. It does not prescribe a fleet’s quantities. Set the decision from local demand, lead-time variability, service target, repair criticality, substitution evidence and carrying/obsolescence cost.
Use Transparent Formulas
Build the worksheet with named inputs instead of invented universal numbers:
Average demand during lead time = average validated demand per time unit × expected replenishment lead time
Reorder point = average demand during lead time + approved safety stock
Safety stock input = a fleet-approved function of demand variability, lead-time variability, target availability and criticality
Order quantity = target stock position − on-hand usable stock − open confirmed supply + backorders/allocated demand
Do not average unlike applications into one demand stream unless interchangeability is verified. Distinguish supplier quoted lead time from actual order-to-receipt history. Exclude quarantined, damaged, unverified and allocated units from usable on-hand stock.
| Worksheet input | Unit | Owner/source | Expected | Conservative | Stress |
|---|---|---|---|---|---|
| Validated demand rate | Units/time | Maintenance + stores | Enter | Enter | Enter |
| Replenishment lead time | Time | Purchasing history | Enter | Enter | Enter |
| Demand variability | Defined measure | Inventory analyst | Enter | Enter | Enter |
| Lead-time variability | Defined measure | Purchasing | Enter | Enter | Enter |
| Criticality/service target | Approved class | Fleet operations | Enter | Enter | Enter |
| Usable on-hand | Units | Cycle count | Enter | Enter | Enter |
| Open confirmed supply | Units/date | Purchase orders | Enter | Enter | Enter |
| Allocated/backordered | Units | Work orders | Enter | Enter | Enter |
| Calculated reorder point | Units | Formula | Calculate | Calculate | Calculate |

Scenario columns expose assumptions without presenting fictional demand rates, lead times or safety-stock quantities.
Control Inventory Risk
Manage Supersession and Change
When an OE or supplier number changes, determine whether replacement direction is one-way or reversible. Compare connector population, pinout, architecture, software, functions, mounting and vehicle evidence before merging stock. Record whether old stock can be consumed, reworked, returned or must be quarantined.
Require change notification for connector/terminal, contact, PCB/firmware, resistor, illumination, housing/tool, mechanism and test-program changes. The manufacturer audit checklist helps verify change control and traceability at the supply source.
Review Slow, Excess and Obsolete Stock
Review fleet population remaining, future removals, demand age, supersession, open orders and application confidence. Do not call a part obsolete only because it has not moved recently; low-frequency critical spares may be intentional. Conversely, an apparently active item can become stranded when the last compatible vehicles leave the fleet.
Use cycle counts and location controls to detect mixed bins. Quarantine returns until identity and condition are established. A fitted or electrically tested switch should not automatically re-enter new stock. Define separate statuses for new, inspected return, warranty hold, diagnostic sample and scrap.
Close the Quality Loop
Link unusual demand to failure evidence by lot, vehicle cohort and repair outcome. Rising thermal damage may require connector/load investigation rather than a larger stock level. Repeated wrong-function returns may reveal application-master errors. Mechanical complaints confined to one revision may justify supplier corrective action and targeted containment.
Review at a defined cadence and after triggers such as a new vehicle introduction, supplier change, major failure trend, long lead-time shift, supersession or fleet disposal. Record the approver and effective date for changes to min/max, reorder point or application scope.
Final Release Checklist
- Every stock ID has a verified orderable number and vehicle boundary.
- OE supersession direction and application evidence are controlled.
- Same-connector parts are not merged without electrical and functional proof.
- Demand excludes known misdiagnosis, returns and duplicate warranty events.
- Observation window, numerator, denominator and exposure are defined.
- Criticality and supply risk are evaluated separately from frequency.
- Reorder inputs use current demand and actual lead-time evidence.
- Usable stock excludes quarantine, damage and allocations.
- Lot/serial evidence is retained at the required traceability level.
- Slow, obsolete and changed parts have documented disposition.
- Failure trends feed diagnosis, supplier action and stock review.
Work With TONFUL
TONFUL’s automotive combination switch range presents current application references. Share fleet vehicle/VIN scope, OE and supplier numbers, annual demand history, confirmed failure modes, lead-time needs and receiving/traceability requirements. TONFUL can support candidate comparison and sample approval; final stocking quantities remain a fleet decision based on verified applications and local operating data.