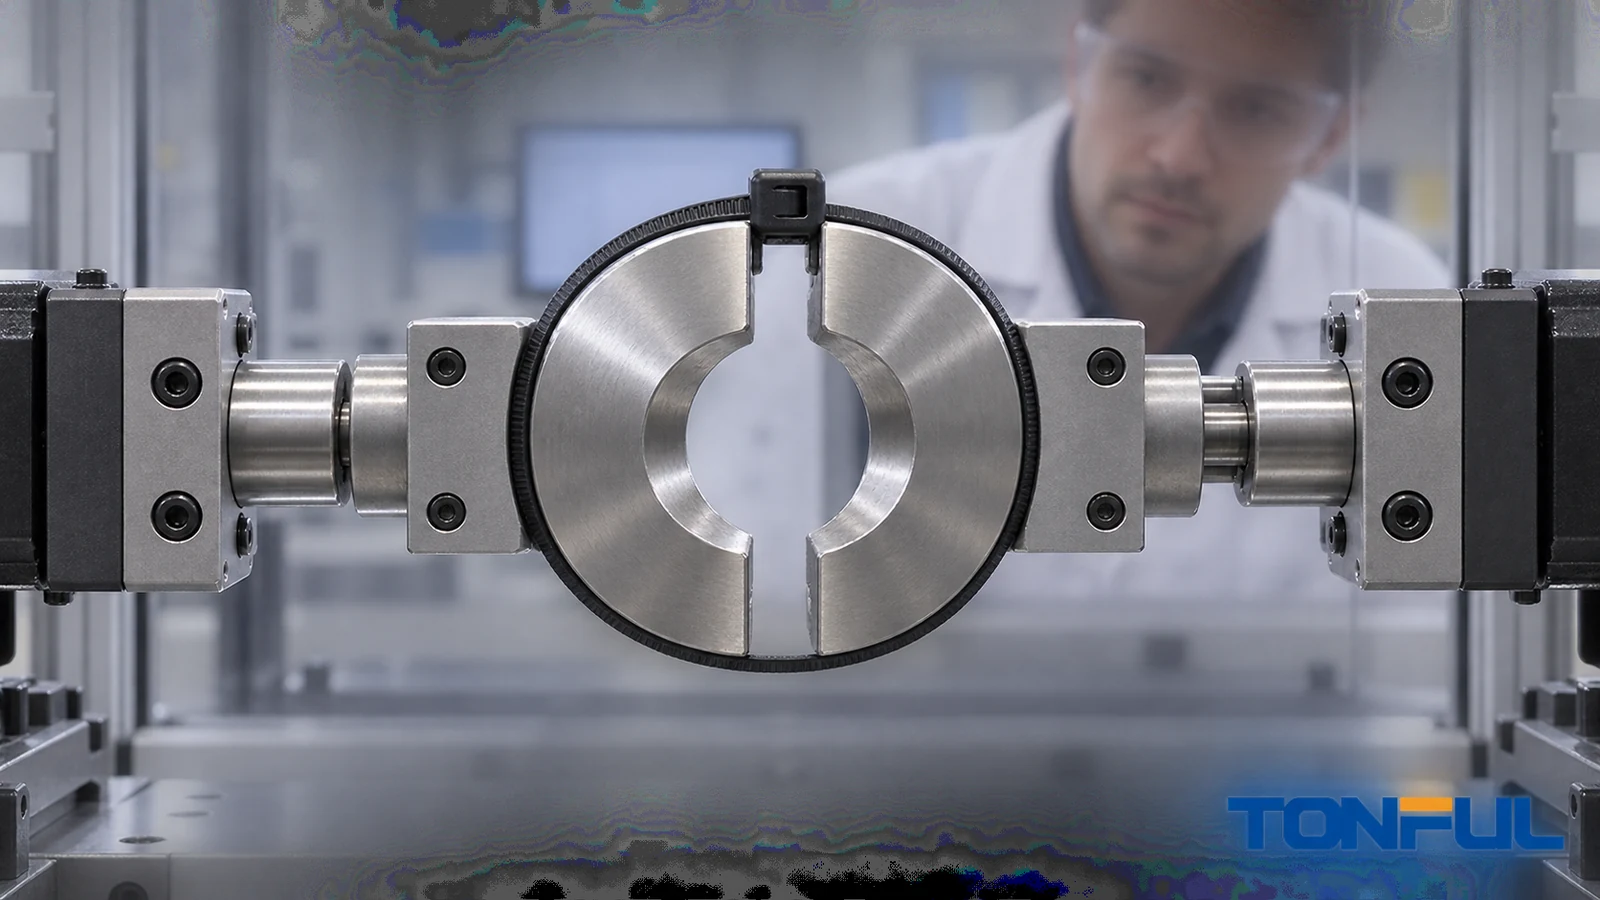
Minimum loop tensile strength is a declared mechanical characteristic of a cable tie after its locking mechanism has been engaged and the closed loop is loaded under a defined test method. It helps buyers compare named products and verify production against an agreed requirement. It is not automatically the allowable working load, safe suspended mass, long-term holding force or strength of a tie-and-mount installation.
That distinction prevents a common error. A catalog may state 50 lbf or approximately 222 N, but this does not mean the tie should support a 50-pound cable bundle continuously. The laboratory fixture, loading rate, conditioning, sample population and failure criterion differ from a real installation exposed to time, temperature, vibration, chemicals and a fixing surface. Use the tensile value as one controlled input, then validate the application separately.
What the Term Means
“Loop” means the strap is fed through its head so the pawl or other locking mechanism is engaged. “Tensile” refers to the opening force applied to that closed loop. “Minimum” normally identifies a declared lower requirement or specification threshold rather than the average result of a few favorable specimens. The exact meaning still depends on the cited standard, product specification and sampling plan.
UL Solutions describes loop tensile strength as a reference characteristic of a cable tie with its locking mechanism engaged. UL’s guidance also separates the tie’s loop-tensile characteristic from the mechanical strength of a fixing device. This matters because a strong strap can be installed on a weak adhesive mount, clip, screw or panel. It also matters when a tie is intended to provide primary support, which has additional product and installation boundaries.
IEC 62275:2022 covers metallic, non-metallic and composite cable ties and associated fixing devices used to manage or secure wiring systems in electrical installations. The official summary notes defined tensile testing and the possibility of dead-weight testing in the current edition. To reproduce or claim conformance, use the purchased standard and its applicable national requirements; this article does not replace the procedure.
| Term | What it can describe | What it does not establish alone |
|---|---|---|
| Individual test result | Force at the defined failure event for one specimen | Lot minimum or field life |
| Sample minimum | Lowest result among tested specimens | Population minimum unless sampling rules say so |
| Declared minimum | Product specification threshold under the cited method | Working load or support approval |
| Average/mean | Arithmetic average of sample results | Assurance that every specimen passes |
| Fixing-device strength | Mount performance under its method | Cable-tie loop strength |
| Installed assembly strength | Tie, mount, fastener and substrate under a defined test | Universal suitability outside that configuration |
How a Loop Tensile Test Works
A typical test closes the tie around a specified split or expanding mandrel fixture. The tie may be installed using a controlled tool and tension. The test machine then separates or expands the fixture at a defined rate while measuring force. The result is recorded at the specified failure event, which might involve strap rupture, tooth damage, head fracture or locking-mechanism release. The actual fixture geometry and procedure must come from the governing method.

The value is meaningful only with its conditions. Nylon properties can be affected by moisture conditioning and temperature. Installation tension can change how the teeth and pawl engage. Test speed and fixture geometry can change stress distribution. A stainless-steel tie can use a different lock and failure mode from a molded polymer tie. Therefore, a result without the test method and specimen identity is incomplete evidence.
Minimum Test Record
| Record field | Required entry |
|---|---|
| Product identity | Manufacturer, full part number, drawing revision and lot |
| Construction | Material, color, dimensions, head and locking design |
| Standard/method | Document, edition, clause or customer procedure |
| Conditioning | Time, temperature, humidity/moisture preparation |
| Sample plan | Quantity, selection basis, exclusions and retest rule |
| Installation | Tool, setting, loop/mandrel geometry and operator |
| Test system | Machine/fixture ID, range, resolution and calibration status |
| Test conditions | Speed, ambient condition and force units |
| Results | Every raw result, failure mode and specimen note |
| Decision | Requirement, pass/fail, reviewer and date |
Do not record only the average. If the requirement is a minimum, every result and the lowest value need visibility. Preserve invalid-test reasons rather than deleting inconvenient results. A specimen damaged by verified handling may justify a documented replacement under the approved plan; an unexpected low result should trigger investigation, not automatic retesting until the lot passes.
Newtons, Pound-Force and Kilograms
Tensile force is commonly reported in newtons (N) or pound-force (lbf). For unit conversion, 1 lbf is approximately 4.448 N. Thus, 50 lbf is approximately 222 N. This conversion only expresses the same force in different units. It does not create a safe payload.
Kilograms measure mass, not force. On Earth, engineers may calculate the gravitational force of a mass using F = m × g, but converting a tensile test result into an equivalent static mass still does not establish permissible service load. The tie may experience creep, shock, vibration, thermal cycling or uneven load sharing. A mount, cable jacket or substrate may fail first. Do not publish “holds X kg” unless a controlled product/application specification defines exactly what that claim means and how it was validated.
The TONFUL tensile-strength guide provides a broader product-selection overview. For purchasing, compare values only when units and test methods match. A “50” in lbf is not equivalent to 50 N, and a breaking-force result from one method may not be equivalent to a withstand requirement from another.
Why It Is Not an Allowable Working Load
A short laboratory tensile test answers a limited question about a specimen. A service load can remain for months or years. Polymer ties can creep under sustained stress, especially as temperature rises. UV, moisture, chemicals and thermal aging can change properties. Dynamic equipment can add acceleration and shock. A tight tie may damage a cable jacket before the strap fails. None of these are resolved by dividing the declared tensile value by bundle weight.
Primary support also depends on the complete load path: tie, fixing device, fastener, substrate and installation. UL notes different considerations for securing and supporting applications. Use the project’s approved support arrangement and electrical rules; do not assume that a higher loop-tensile number upgrades an ordinary tie into a support device. The relevant TONFUL application discussion is in the cable-tie use guide, while exact support approval remains product- and site-specific.
Even for simple bundling, “stronger” may not be better. A wide, high-strength tie tightened around delicate data cable can create excessive pressure. A lower-profile tie or reusable wrap may suit maintenance access. Selection should balance bundle diameter, routing, jacket sensitivity, environment and tool control rather than maximizing one number.
How Buyers Should Compare Datasheets
First, compare exact part numbers rather than product-family headlines. Record material, width, length, head design, usable bundle range and test value. Confirm whether the number is minimum, typical, nominal, average or a single result. Ask which standard edition and conditioning method apply. A supplier’s internal method can be useful for process control, but it should not be presented as equivalent to a customer or certification method without a documented comparison.
Second, separate certification from a marketing table. If a certified value is required, verify the exact listing or certificate scope and current production model. Do not infer that every color, material option or custom version is covered. The TONFUL cable-tie manufacturing guide describes process stages that can influence consistency, but no general process description proves a specific lot’s tensile result.
Third, assess whether the sample represents production. Pre-production pieces, conditioned laboratory samples and aged stock may behave differently. Require lot identity and retain samples where the project needs traceability. Nylon storage and moisture condition should be controlled; the TONFUL moisture and storage guide explains why handling history belongs in the investigation.
| Comparison question | Acceptable evidence | Warning sign |
|---|---|---|
| Is the same property being compared? | Same test method/edition and failure definition | “Heavy duty” with no method |
| Is the requirement a true minimum? | All specimen data and clear threshold | Only average or best result shown |
| Does the sample match the order? | Part, material, color, lot and revision traceability | Generic family report |
| Are units correct? | N and/or lbf clearly labeled | “lb” or “kg” used ambiguously |
| Are conditions controlled? | Conditioning, speed, fixture and tool recorded | Unconditioned hand pull |
| Is the field claim separate? | Application validation and load path documented | Tensile value called safe working load |
Lot Inspection and Process Capability
Incoming inspection should follow an agreed sampling and reaction plan. Verify packaging, part identity and dimensions before destructive tensile testing. Randomly select specimens across cartons or production positions as defined. Test using controlled conditioning and calibrated equipment. Record all values and failure modes, then quarantine the lot if the acceptance rule is not met. Supplier and customer should agree how replacement samples, invalid tests and corrective action are handled before testing begins.
A passing sample does not prove every unit in a large lot, and one failed specimen should not be hidden by a high average. For stable high-volume production, review distribution and process capability only when the process is statistically controlled and specification limits are legitimate. Cp or Cpk cannot rescue mixed data, uncalibrated equipment or a one-sided result with an undefined lower limit. Trend by mold cavity, machine, material batch or shift when those factors are relevant.
Failure mode carries useful information. Strap rupture in a consistent zone may suggest a geometry or material issue; tooth stripping may point toward engagement, installation tension or molding; head cracking may indicate stress concentration; lock release may involve design or assembly. These are investigation directions, not universal diagnoses. Confirm through dimensions, material records, molding data and repeatable tests. The TONFUL cold-weather guide can inform environmental questions, but it does not set a universal root cause for a low room-temperature result.

A Practical RFQ and Approval Checklist
An RFQ should state exact tie dimensions and material, bundle range, required minimum loop tensile strength, units, test method/edition, conditioning, sample quantity, reporting format and lot-acceptance rule. Add operating environment, installation temperature, tool and tension requirement, fixing device and certification scope. If the tie is part of a support assembly, specify that function separately and include mount, fastener, substrate and application validation.
Ask for a controlled drawing, product-specific report, certificate/listing where required, and production samples. Approve the named construction rather than a generic “50-lb tie.” Define change notification for resin grade, color concentrate, mold, head geometry, manufacturing site and test method. The TONFUL cable-ties product range can begin the discussion; TONFUL should provide exact-product evidence before any value is used in a customer specification.
Work With TONFUL
Send TONFUL the bundle geometry, environment, tie function, required test method, minimum value, sampling plan and documentation expectations. Ask for results in both the original unit and any clearly labeled conversion, with every specimen and failure mode visible. Do not ask TONFUL to turn a loop-tensile value into an unsupported working-load promise. Final approval should combine the named tie’s verified test evidence with the actual installation, maintenance and failure-consequence requirements.
Technical Sources
- UL Solutions, Cable Ties for Cable Management: definition and boundary of loop tensile strength, fixing-device strength and support classifications.
- IEC 62275:2022: official scope for cable ties and fixing devices and current-edition tensile-test context.